

ISO 21809-3
(Main)Oil and gas industries including lower carbon energy — External coatings for buried or submerged pipelines used in pipeline transportation systems — Part 3: Field joint coatings
- Abstract
ISO 21809-3:2016 specifies requirements for field joint coating of seamless or welded steel pipes for buried and submerged sections of pipeline transportation systems used in the petroleum, petrochemical and natural gas industries as defined in ISO 13623. This part of ISO 21809 specifies the qualification, application and testing of the corrosion protection coatings applied to steel surfaces left bare after the joining of pipes and fittings (components) by welding. ISO 21809-3:2016 defines and codifies in Table 1 the different types of field joint coatings for pipelines. ISO 21809-3:2016 does not address requirements for additional mechanical protection, for thermal insulation or for joint infills of concrete weight-coated pipes. NOTE Field joints of pipes and fittings coated in accordance with this part of ISO 21809 are considered suitable for further protection by means of cathodic protection.
- Status
- Not Published
- Technical Committee
- ISO/TC 67/SC 2 - Pipeline transportation systems
- Drafting Committee
- ISO/TC 67/SC 2/WG 14 - External pipeline protective coatings
- Current Stage
- 6000 - International Standard under publication
- Start Date
- 17-Nov-2026
- Completion Date
- 21-Nov-2026
Buy Documents
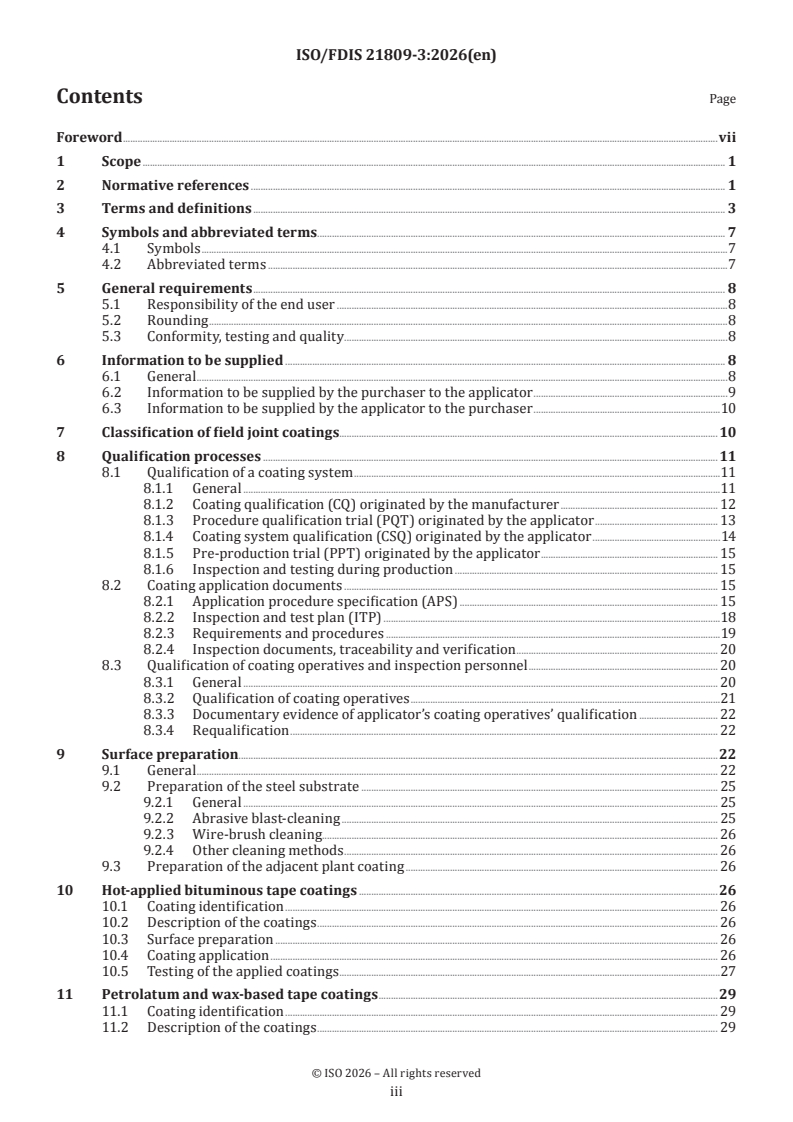
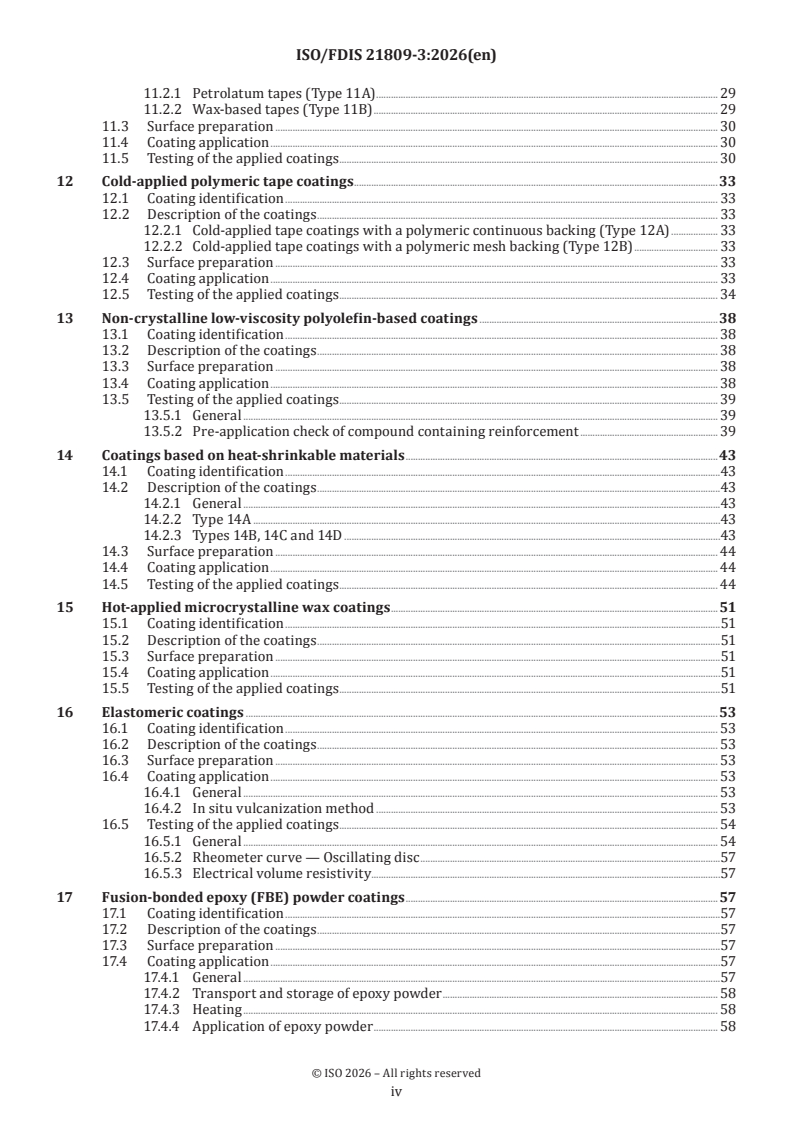
ISO/FDIS 21809-3 - Oil and gas industries including lower carbon energy — External coatings for buried or submerged pipelines used in pipeline transportation systems — Part 3: Field joint coatings
REDLINE ISO/FDIS 21809-3 - Oil and gas industries including lower carbon energy — External coatings for buried or submerged pipelines used in pipeline transportation systems — Part 3: Field joint coatings
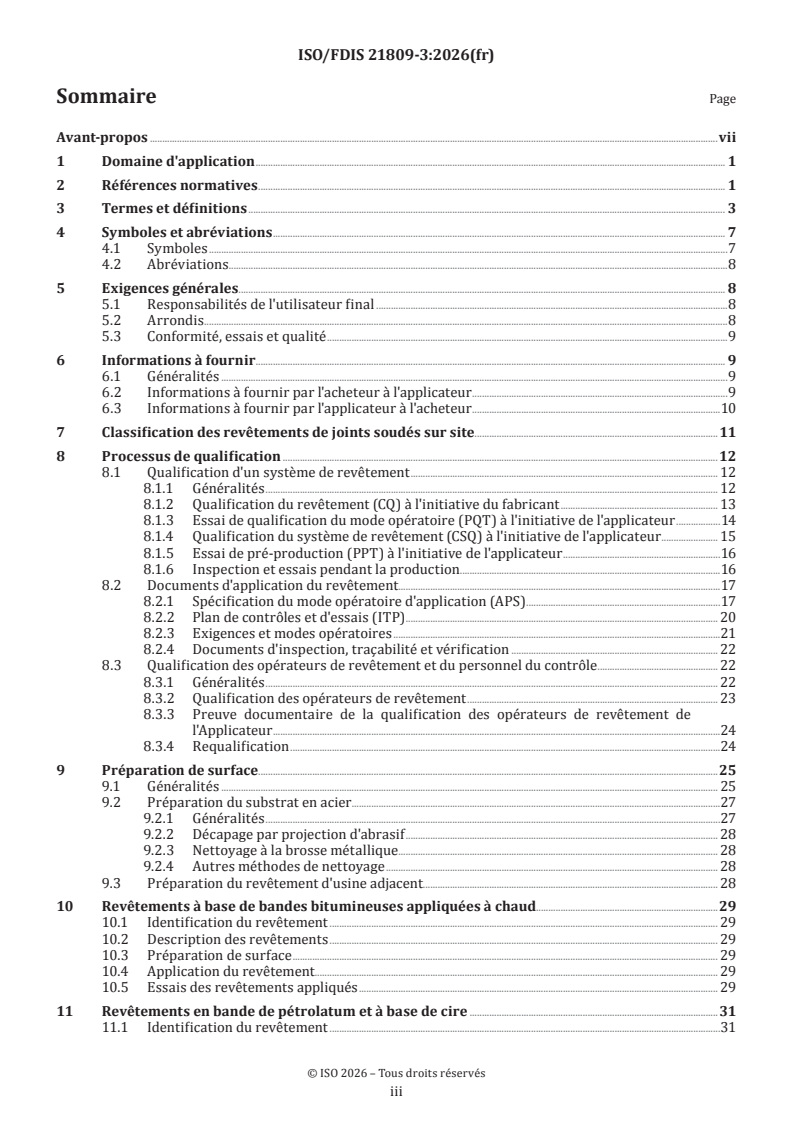
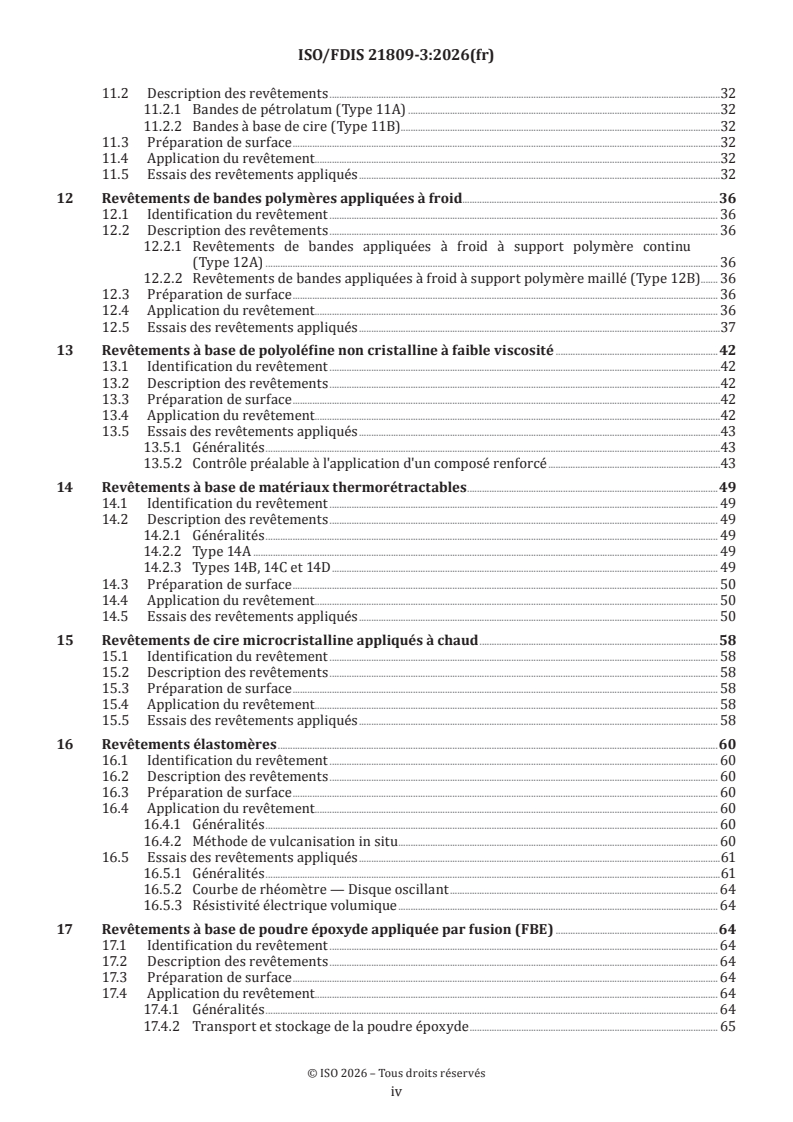
ISO/FDIS 21809-3 - Industries du pétrole et du gaz, y compris les énergies à faible teneur en carbone — Revêtements externes des conduites enterrées ou immergées utilisées dans les systèmes de transport par conduites — Partie 3: Revêtements des joints soudés sur site
ISO 21809-3 is an ISO standard for field joint coatings on seamless or welded steel pipes used in buried or submerged sections of pipeline transportation systems in the petroleum, petrochemical and natural gas industries. It specifies how these corrosion protection coatings are qualified, applied and tested for the bare steel left after welding, so purchasers, applicators and inspectors can agree what the field joint coating must do.
What does ISO 21809-3 specify?
ISO 21809-3 specifies requirements for field joint coating of steel pipes for buried and submerged pipeline sections. It covers the qualification, application and testing of coatings applied to the steel surfaces left bare at welded joints.
ISO 21809-3 also defines and codifies the field joint coating types in Table 1, so users can match a coating system to the correct clause. It does not cover additional mechanical protection, thermal insulation, or joint infills of concrete weight-coated pipes.
The document is organized into clauses 1 to 20, followed by normative annexes A to R.
| Annex | What it covers |
|---|---|
| A | Reporting of results |
| B | Inspection of thickness |
| C | Holiday detection test |
| D | Impact test |
| E | Indentation test |
| F | Specific electrical insulation resistance test |
| G | Cathodic disbondment test |
| H | Adhesion test, including peel, lift and pull off |
| I | Hot water immersion test |
| J | Lap shear test |
| K | Drip resistance test |
| L | Peel strength between layers |
| M | Thermal ageing resistance |
| N | Coating porosity test |
| O | Bursting strength of reinforced backing |
| P | Thermal analysis of epoxy powder and cured coating film (FBE) |
| Q | Adhesion test (X cut) - resistance to removal |
| R | Coating flexibility test |
What are the key requirements of ISO 21809-3?
ISO 21809-3 is built around one central idea: the field joint coating system must be defined, qualified, applied under controlled conditions, and verified by test methods matched to the coating type. In practice, the standard makes the purchaser, applicator and end user agree the coating system and its acceptance route before production starts.
Classification of field joint coatings
Clause 7 classifies the field joint coatings in Table 1. The list spans hot-applied tapes, petrolatum and wax-based tapes, cold-applied polymeric tapes, non-crystalline low-viscosity polyolefin-based coatings, heat-shrinkable systems, microcrystalline wax, elastomeric coatings, fusion-bonded epoxy (FBE) powder coatings, liquid-applied coatings, hot-applied polyolefin-based and polyurethane coatings, and thermal spray aluminium (TSA) coatings.
This classification matters because each family has its own surface preparation, application method and acceptance tests. A buyer or engineer can use the clause number and code in Table 1 to select the right system without mixing requirements from different coating families.
Qualification and production control
Clause 8 sets out qualification processes for coating systems. It includes coating qualification (CQ) from the manufacturer, procedure qualification trial (PQT) and coating system qualification (CSQ) from the applicator, and pre-production trial (PPT) before production starts.
Clause 8 also requires coating application documents. The application procedure specification (APS) describes the methods, equipment and tools for application, while the inspection and test plan (ITP) sets out the inspection sequence, resources and procedure references. In practice, these documents are the control point for the job: they define what will be done, by whom, and when it will be checked.
Clause 8 additionally covers qualification of coating operatives and inspection personnel. That matters because the standard does not treat field coating as a generic shop activity - it expects the people doing the work and the inspections to be qualified for the system being used.
Surface preparation before coating
Clause 9 controls the state of the steel before coating. It covers preparation of the steel substrate and the adjacent plant coating, including cleanliness grade, surface profile, dust, and soluble salts.
Table 3 links these surface preparation requirements to the FJC type. The standard distinguishes between hand and power tool cleaning, abrasive blast cleaning, and the cleanliness level needed for each coating family. It also ties surface profile and salt limits to the coating type.
This is important in practice because field joint failures often start at the interface. The standard makes the surface condition part of the acceptance criteria, not just a workmanship note.
Coating family clauses and their tests
Clauses 10 to 20 each cover one coating family. Every family section follows the same pattern: coating identification, description, surface preparation, coating application, and testing of the applied coating.
That structure helps users compare systems, but the actual tests differ by family. For example, the document uses holiday detection, impact resistance, peel strength, cathodic disbondment, indentation resistance, specific electrical insulation resistance, and hot water immersion in different combinations depending on the coating type.
Some families also use extra methods for their specific behavior. Examples include drip resistance for wax and bituminous systems, peel strength between layers for multi-layer tapes and heat-shrinkable systems, thermal ageing resistance, porosity checks, bursting strength for reinforced backing, thermal analysis for FBE, X-cut adhesion, and flexibility testing.
Reporting and traceability
Annex A gives the rules for reporting results. Clause 8 also requires inspection documents, traceability and verification, with inspection documents issued in accordance with ISO 10474 or EN 10204.
In practice, this means the coating job is not only a material and application exercise - it also has to leave a documented record that shows the coating batch, the test results, and the conformity statement for the purchase order.
What terms does ISO 21809-3 define?
- application procedure specification (APS) - A document that describes the procedures, methods, equipment and tools used for field joint coating application.
- inspection and testing plan (ITP) - A document that shows the sequence of inspections and tests, including the resources and procedure references used for the job.
- procedure qualification trial (PQT) - An application trial carried out at the applicator’s premises or another agreed location to confirm that the APS and ITP can produce acceptable properties.
- pre-production trial (PPT) - An application and test trial done immediately before production to confirm that the specified properties can be achieved in production conditions.
- coating system - One layer or several layers of coating material applied to metal to keep electrolyte away from the surface and prevent corrosion.
- field joint area - The uncoated area created when pipe sections or fittings with cutbacks are welded together in the field.
- holiday - A coating discontinuity that becomes electrically conductive when a specified voltage is applied.
- maximum service temperature (T) - The maximum continuous temperature that the field joint coating can resist.
Who uses ISO 21809-3?
ISO 21809-3 is used by end users, purchasers, applicators, manufacturers, inspectors and coating operatives involved with pipeline coatings. It is relevant to pipeline transportation systems in the petroleum, petrochemical and natural gas industries, including lower carbon energy applications covered by the series title.
In practice, end users and purchasers use it to specify the coating system and acceptance requirements, applicators use it to prepare APS and ITP documents and carry out work, manufacturers use it to qualify coating materials, and inspectors use it to verify thickness, holidays, adhesion and the other required tests.
What changed in ISO 21809-3 from the previous edition?
The foreword says this third edition cancels and replaces ISO 21809-3:2016 and incorporates ISO 21809-3:2016/Amd 1:2020.
The main changes listed are:
- inclusion of a qualification scheme
- inclusion of new FJC types
- changes in various FJC clauses
- inclusion of new annexes
- changes in various annexes
Which standards are used with ISO 21809-3?
Clause 2 cites many standards and technical documents that support surface preparation, material testing, inspection and coating qualification.
- ISO 13623 and ISO 3183 - define the pipeline transportation context and the steel pipe used in these systems.
- ISO 8501-1, ISO 8501-3, ISO 8502-3, ISO 8502-6, ISO 8502-9, ISO 8503-4, ISO 8503-5, ISO 8504-2, ISO 8504-3 - support steel surface preparation, cleanliness assessment and surface profile measurement.
- ISO 10474 and EN 10204 - support inspection documents and conformity records.
- ISO/IEC 17025 - supports competence of testing and calibration laboratories.
- ISO 34-1, ISO 37, ISO 48-4, ISO 188, ISO 527-1, ISO 527-2, ISO 527-3, ISO 868, ISO 1431-1, ISO 1817, ISO 3303-1, ISO 3417, ISO 4624, ISO 5893, ISO 7619-1, ISO 11357-1, ISO 11357-2, ISO 11357-3, ISO 11357-6 - provide material test methods used for rubber, plastics, adhesion, cure behavior, hardness, tear, tensile properties and thermal analysis.
- ASTM D70, ASTM D92, ASTM D127, ASTM D149, ASTM D1141, ASTM D1321, ASTM D2084, ASTM D4285, ASTM D4940 - provide additional test methods used for specific coating materials and test conditions.
- AWS C2.25/C2.25M, SSPC-SP1, SSPC Guide 15, SSPC CS 23.00 - support thermal spray feedstock, solvent cleaning, soluble salt extraction and TSA application practice.
What does the ISO 21809-3 document contain?
ISO 21809-3 contains the full set of coating-family clauses and a large set of test annexes for field joint coatings. The annexes give the practical methods for measuring thickness, holidays, impact, indentation, insulation resistance, cathodic disbondment, adhesion, hot water immersion, lap shear, drip resistance, peel strength between layers, thermal ageing, porosity, bursting strength, thermal analysis, X-cut adhesion and flexibility.
It also includes figures and procedures for the test setups, such as the equipment for holiday detection, cathodic disbondment cells, peel strength rigs, lap shear specimens and flexibility bending devices. These annexes are the parts most often used in qualification, production testing and dispute checks, because they define how to prepare the sample, run the test and record the result.
The document also contains detailed tables of requirements and test frequencies for each coating family. Those tables are the practical core of the standard: they tell the user which test applies to which FJC type, when to test it, and what property the result is meant to confirm.
Relations
- Effective Date
- 12-Feb-2026
- Effective Date
- 26-Apr-2025
- Effective Date
- 26-Apr-2025
Buy Documents
ISO/FDIS 21809-3 - Oil and gas industries including lower carbon energy — External coatings for buried or submerged pipelines used in pipeline transportation systems — Part 3: Field joint coatings
REDLINE ISO/FDIS 21809-3 - Oil and gas industries including lower carbon energy — External coatings for buried or submerged pipelines used in pipeline transportation systems — Part 3: Field joint coatings
ISO/FDIS 21809-3 - Industries du pétrole et du gaz, y compris les énergies à faible teneur en carbone — Revêtements externes des conduites enterrées ou immergées utilisées dans les systèmes de transport par conduites — Partie 3: Revêtements des joints soudés sur site
Get Certified
Connect with accredited certification bodies for this standard
Element Materials Technology
Materials testing and product certification.

ABS Group Brazil
ABS Group certification services in Brazil.
ABS Quality Evaluations Inc.
American Bureau of Shipping quality certification.
Sponsored listings
Frequently Asked Questions
ISO 21809-3 is a draft published by the International Organization for Standardization (ISO). Its full title is "Oil and gas industries including lower carbon energy — External coatings for buried or submerged pipelines used in pipeline transportation systems — Part 3: Field joint coatings". This standard covers: ISO 21809-3:2016 specifies requirements for field joint coating of seamless or welded steel pipes for buried and submerged sections of pipeline transportation systems used in the petroleum, petrochemical and natural gas industries as defined in ISO 13623. This part of ISO 21809 specifies the qualification, application and testing of the corrosion protection coatings applied to steel surfaces left bare after the joining of pipes and fittings (components) by welding. ISO 21809-3:2016 defines and codifies in Table 1 the different types of field joint coatings for pipelines. ISO 21809-3:2016 does not address requirements for additional mechanical protection, for thermal insulation or for joint infills of concrete weight-coated pipes. NOTE Field joints of pipes and fittings coated in accordance with this part of ISO 21809 are considered suitable for further protection by means of cathodic protection.
ISO 21809-3:2016 specifies requirements for field joint coating of seamless or welded steel pipes for buried and submerged sections of pipeline transportation systems used in the petroleum, petrochemical and natural gas industries as defined in ISO 13623. This part of ISO 21809 specifies the qualification, application and testing of the corrosion protection coatings applied to steel surfaces left bare after the joining of pipes and fittings (components) by welding. ISO 21809-3:2016 defines and codifies in Table 1 the different types of field joint coatings for pipelines. ISO 21809-3:2016 does not address requirements for additional mechanical protection, for thermal insulation or for joint infills of concrete weight-coated pipes. NOTE Field joints of pipes and fittings coated in accordance with this part of ISO 21809 are considered suitable for further protection by means of cathodic protection.
ISO 21809-3 is classified under the following ICS (International Classification for Standards) categories: 75.200 - Petroleum products and natural gas handling equipment. The ICS classification helps identify the subject area and facilitates finding related standards.
ISO 21809-3 has the following relationships with other standards: It is inter standard links to FprEN ISO 21809-3, ISO 21809-3:2016/Amd 1:2020, ISO 21809-3:2016. Understanding these relationships helps ensure you are using the most current and applicable version of the standard.
ISO 21809-3 is available in PDF format for immediate download after purchase. The document can be added to your cart and obtained through the secure checkout process. Digital delivery ensures instant access to the complete standard document.
Standards Content (Sample)
FINAL DRAFT
International
Standard
ISO/FDIS 21809-3
ISO/TC 67/SC 2
Oil and gas industries including
Secretariat: UNI
lower carbon energy — External
Voting begins on:
coatings for buried or submerged
2026-09-21
pipelines used in pipeline
Voting terminates on:
transportation systems —
2026-11-16
Part 3:
Field joint coatings
Industries du pétrole et du gaz, y compris les énergies à faible
teneur en carbone — Revêtements externes des conduites
enterrées ou immergées utilisées dans les systèmes de transport
par conduites —
Partie 3: Revêtements des joints réalisés sur site
RECIPIENTS OF THIS DRAFT ARE INVITED TO SUBMIT,
WITH THEIR COMMENTS, NOTIFICATION OF ANY
RELEVANT PATENT RIGHTS OF WHICH THEY ARE AWARE
AND TO PROVIDE SUPPOR TING DOCUMENTATION.
IN ADDITION TO THEIR EVALUATION AS
BEING ACCEPTABLE FOR INDUSTRIAL, TECHNO-
ISO/CEN PARALLEL PROCESSING LOGICAL, COMMERCIAL AND USER PURPOSES, DRAFT
INTERNATIONAL STANDARDS MAY ON OCCASION HAVE
TO BE CONSIDERED IN THE LIGHT OF THEIR POTENTIAL
TO BECOME STAN DARDS TO WHICH REFERENCE MAY BE
MADE IN NATIONAL REGULATIONS.
Reference number
ISO/FDIS 21809-3:2026(en) © ISO 2026
FINAL DRAFT
ISO/FDIS 21809-3:2026(en)
International
Standard
ISO/FDIS 21809-3
ISO/TC 67/SC 2
Oil and gas industries including
Secretariat: UNI
lower carbon energy — External
Voting begins on:
coatings for buried or submerged
pipelines used in pipeline
Voting terminates on:
transportation systems —
Part 3:
Field joint coatings
Industries du pétrole et du gaz, y compris les énergies à faible
teneur en carbone — Revêtements externes des conduites
enterrées ou immergées utilisées dans les systèmes de transport
par conduites —
Partie 3: Revêtements des joints réalisés sur site
RECIPIENTS OF THIS DRAFT ARE INVITED TO SUBMIT,
WITH THEIR COMMENTS, NOTIFICATION OF ANY
RELEVANT PATENT RIGHTS OF WHICH THEY ARE AWARE
AND TO PROVIDE SUPPOR TING DOCUMENTATION.
© ISO 2026
IN ADDITION TO THEIR EVALUATION AS
All rights reserved. Unless otherwise specified, or required in the context of its implementation, no part of this publication may
BEING ACCEPTABLE FOR INDUSTRIAL, TECHNO-
ISO/CEN PARALLEL PROCESSING
LOGICAL, COMMERCIAL AND USER PURPOSES, DRAFT
be reproduced or utilized otherwise in any form or by any means, electronic or mechanical, including photocopying, or posting on
INTERNATIONAL STANDARDS MAY ON OCCASION HAVE
the internet or an intranet, without prior written permission. Permission can be requested from either ISO at the address below
TO BE CONSIDERED IN THE LIGHT OF THEIR POTENTIAL
or ISO’s member body in the country of the requester.
TO BECOME STAN DARDS TO WHICH REFERENCE MAY BE
MADE IN NATIONAL REGULATIONS.
ISO copyright office
CP 401 • Ch. de Blandonnet 8
CH-1214 Vernier, Geneva
Phone: +41 22 749 01 11
Email: copyright@iso.org
Website: www.iso.org
Published in Switzerland Reference number
ISO/FDIS 21809-3:2026(en) © ISO 2026
ii
ISO/FDIS 21809-3:2026(en)
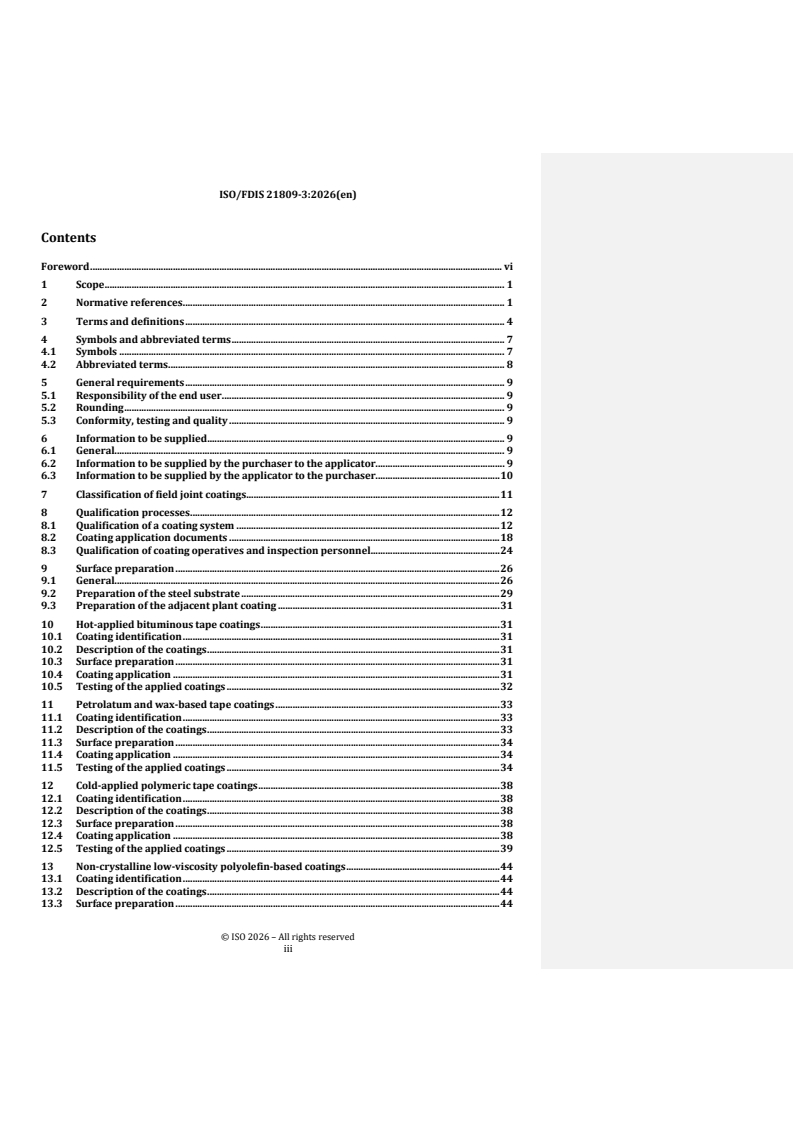
Contents Page
Foreword .vii
1 Scope . 1
2 Normative references . 1
3 Terms and definitions . 3
4 Symbols and abbreviated terms. 7
4.1 Symbols .7
4.2 Abbreviated terms .7
5 General requirements . 8
5.1 Responsibility of the end user .8
5.2 Rounding .8
5.3 Conformity, testing and quality . . .8
6 Information to be supplied . 8
6.1 General .8
6.2 Information to be supplied by the purchaser to the applicator .9
6.3 Information to be supplied by the applicator to the purchaser .10
7 Classification of field joint coatings. 10
8 Qualification processes .11
8.1 Qualification of a coating system .11
8.1.1 General .11
8.1.2 Coating qualification (CQ) originated by the manufacturer . 12
8.1.3 Procedure qualification trial (PQT) originated by the applicator . 13
8.1.4 Coating system qualification (CSQ) originated by the applicator .14
8.1.5 Pre-production trial (PPT) originated by the applicator . 15
8.1.6 Inspection and testing during production . 15
8.2 Coating application documents . 15
8.2.1 Application procedure specification (APS) . 15
8.2.2 Inspection and test plan (ITP) .18
8.2.3 Requirements and procedures .19
8.2.4 Inspection documents, traceability and verification . 20
8.3 Qualification of coating operatives and inspection personnel . 20
8.3.1 General . 20
8.3.2 Qualification of coating operatives .21
8.3.3 Documentary evidence of applicator’s coating operatives’ qualification . 22
8.3.4 Requalification . 22
9 Surface preparation.22
9.1 General . 22
9.2 Preparation of the steel substrate . 25
9.2.1 General . 25
9.2.2 Abrasive blast-cleaning . 25
9.2.3 Wire-brush cleaning. 26
9.2.4 Other cleaning methods . 26
9.3 Preparation of the adjacent plant coating . 26
10 Hot-applied bituminous tape coatings .26
10.1 Coating identification . 26
10.2 Description of the coatings . 26
10.3 Surface preparation . 26
10.4 Coating application . 26
10.5 Testing of the applied coatings .27
11 Petrolatum and wax-based tape coatings .29
11.1 Coating identification . 29
11.2 Description of the coatings . 29
iii
ISO/FDIS 21809-3:2026(en)
11.2.1 Petrolatum tapes (Type 11A) . 29
11.2.2 Wax-based tapes (Type 11B) . 29
11.3 Surface preparation . 30
11.4 Coating application . 30
11.5 Testing of the applied coatings . . 30
12 Cold-applied polymeric tape coatings .33
12.1 Coating identification . 33
12.2 Description of the coatings . 33
12.2.1 Cold-applied tape coatings with a polymeric continuous backing (Type 12A) . 33
12.2.2 Cold-applied tape coatings with a polymeric mesh backing (Type 12B) . 33
12.3 Surface preparation . 33
12.4 Coating application . 33
12.5 Testing of the applied coatings . 34
13 Non-crystalline low-viscosity polyolefin-based coatings .38
13.1 Coating identification . 38
13.2 Description of the coatings . 38
13.3 Surface preparation . 38
13.4 Coating application . 38
13.5 Testing of the applied coatings . . 39
13.5.1 General . 39
13.5.2 Pre-application check of compound containing reinforcement . 39
14 Coatings based on heat-shrinkable materials .43
14.1 Coating identification .43
14.2 Description of the coatings .43
14.2.1 General .43
14.2.2 Type 14A .43
14.2.3 Types 14B, 14C and 14D .43
14.3 Surface preparation . 44
14.4 Coating application . 44
14.5 Testing of the applied coatings . 44
15 Hot-applied microcrystalline wax coatings . 51
15.1 Coating identification .51
15.2 Description of the coatings .51
15.3 Surface preparation .51
15.4 Coating application .51
15.5 Testing of the applied coatings .51
16 Elastomeric coatings .53
16.1 Coating identification . 53
16.2 Description of the coatings . 53
16.3 Surface preparation . 53
16.4 Coating application . 53
16.4.1 General . 53
16.4.2 In situ vulcanization method . 53
16.5 Testing of the applied coatings . 54
16.5.1 General . 54
16.5.2 Rheometer curve — Oscillating disc .57
16.5.3 Electrical volume resistivity.57
17 Fusion-bonded epoxy (FBE) powder coatings .57
17.1 Coating identification .57
17.2 Description of the coatings .57
17.3 Surface preparation .57
17.4 Coating application .57
17.4.1 General .57
17.4.2 Transport and storage of epoxy powder . 58
17.4.3 Heating . 58
17.4.4 Application of epoxy powder . 58
iv
ISO/FDIS 21809-3:2026(en)
17.5 Testing of the applied coatings . 58
17.5.1 General . 58
17.5.2 Thickness . 58
18 Liquid-applied coatings . 61
18.1 Coating identification .61
18.2 Description of the coatings .61
18.2.1 Liquid epoxy — 18A .61
18.2.2 Liquid polyurethane — 18B .61
18.2.3 Fibre reinforced epoxy — 18C .61
18.2.4 Fibre reinforced vinylester — 18D .61
18.2.5 Fibre reinforced polyurethane — 18E .61
18.2.6 Polyolefin enclosure with polyurethane filling — 18F .61
18.3 Surface preparation .61
18.4 Coating application .61
18.4.1 General .61
18.4.2 Heating .62
18.4.3 Liquid coating application . .62
18.4.4 General guideline .62
18.5 Testing of the applied coatings . .62
19 Hot-applied polyolefin-based and polyurethane coatings .66
19.1 Coating identification . 66
19.2 Description of the coatings . 66
19.2.1 Coatings based on flame-sprayed polypropylene powder applied over an epoxy
layer— Type 19A . 66
19.2.2 Coatings based on polypropylene tapes/sheets / extruded hot-applied over an
epoxy layer— Type 19B. 66
19.2.3 Coatings based on injection-moulded polypropylene over an epoxy layer—
Type 19C . 66
19.2.4 Coatings based on flame-sprayed polyethylene powder applied over an epoxy
layer — Type 19D . 66
19.2.5 Coatings based on polyethylene tapes/sheets / extruded hot-applied over an
epoxy layer — Type 19E . . . .67
19.2.6 Coatings based on injection-moulded polyethylene over an epoxy layer —
Type 19F .67
19.2.7 Coatings based on injection-moulded polyurethane over an epoxy or a
polyurethane primer layer — Type 19G.67
19.3 Surface preparation .67
19.4 Coating application .67
19.4.1 General .67
19.4.2 Heating . 68
19.4.3 Application of the primer . 68
19.4.4 Application of the chemically modified PP or PE . . 68
19.4.5 Application of the top coat . 68
19.5 Testing of the applied coatings . 69
20 Thermal spray aluminium (TSA) coatings . 74
20.1 Coating identification .74
20.2 Description of the coatings .74
20.3 Surface preparation .74
20.4 Coating application .74
20.4.1 General .74
20.4.2 Aluminium .74
20.4.3 Sealer .74
20.5 Testing of the applied coatings . 75
Annex A (normative) Reporting of results .77
Annex B (normative) Inspection of thickness .81
Annex C (normative) Holiday detection test .83
v
ISO/FDIS 21809-3:2026(en)
Annex D (normative) Impact test .85
Annex E (normative) Indentation test .93
Annex F (normative) Specific electrical insulation resistance test .96
Annex G (normative) Cathodic disbondment test .107
Annex H (normative) Adhesion test (peel, lift and pull off) .120
Annex I (normative) Hot water immersion test . .131
Annex J (normative) Lap shear test . 134
Annex K (normative) Drip resistance test .137
Annex L (normative) Peel strength between layers .138
Annex M (normative) Thermal ageing resistance .141
Annex N (normative) Coating porosity test . .146
Annex O (normative) Bursting strength of reinforced backing .148
Annex P (normative) Thermal analysis of epoxy powder and cured coating film (FBE) .149
Annex Q (normative) Adhesion test (X cut) — Resistance to removal .156
Annex R (normative) Coating flexibility test . 158
Bibliography .165
vi
ISO/FDIS 21809-3:2026(en)
Foreword
ISO (the International Organization for Standardization) is a worldwide federation of national standards
bodies (ISO member bodies). The work of preparing International Standards is normally carried out through
ISO technical committees. Each member body interested in a subject for which a technical committee
has been established has the right to be represented on that committee. International organizations,
governmental and non-governmental, in liaison with ISO, also take part in the work. ISO collaborates closely
with the International Electrotechnical Commission (IEC) on all matters of electrotechnical standardization.
The procedures used to develop this document and those intended for its further maintenance are described
in the ISO/IEC Directives, Part 1. In particular, the different approval criteria needed for the different types
of ISO document should be noted. This document was drafted in accordance with the editorial rules of the
ISO/IEC Directives, Part 2 (see www.iso.org/directives).
ISO draws attention to the possibility that the implementation of this document may involve the use of (a)
patent(s). ISO takes no position concerning the evidence, validity or applicability of any claimed patent
rights in respect thereof. As of the date of publication of this document, ISO had not received notice of (a)
patent(s) which may be required to implement this document. However, implementers are cautioned that
this may not represent the latest information, which may be obtained from the patent database available at
www.iso.org/patents. ISO shall not be held responsible for identifying any or all such patent rights.
Any trade name used in this document is information given for the convenience of users and does not
constitute an endorsement.
For an explanation of the voluntary nature of standards, the meaning of ISO specific terms and expressions
related to conformity assessment, as well as information about ISO's adherence to the World Trade
Organization (WTO) principles in the Technical Barriers to Trade (TBT), see www.iso.org/iso/foreword.html.
This document was prepared by Technical Committee ISO/TC 67, Oil and gas industries including lower
carbon energy, Subcommittee SC 2, Pipeline transportation systems, in collaboration with the European
Committee for Standardization (CEN) Technical Committee CEN/TC 12, Oil and gas industries including lower
carbon energy, in accordance with the Agreement on technical cooperation between ISO and CEN (Vienna
Agreement).
This third edition cancels and replaces the second edition (ISO 21809-3:2016), which has been technically
revised. It also incorporates the Amendment ISO 21809-3:2016/Amd 1:2020.
The main changes are as follows:
— inclusion of a qualification scheme;
— inclusion of new FJC types;
— changes in various FJC clauses;
— inclusion of new annexes;
— changes in various annexes.
A list of all parts in the ISO 21809 series can be found on the ISO website.
Any feedback or questions on this document should be directed to the user’s national standards body. A
complete listing of these bodies can be found at www.iso.org/members.html.
vii
FINAL DRAFT International Standard ISO/FDIS 21809-3:2026(en)
Oil and gas industries including lower carbon energy —
External coatings for buried or submerged pipelines used in
pipeline transportation systems —
Part 3:
Field joint coatings
1 Scope
This document specifies requirements for field joint coatings of seamless or welded steel pipes for buried
and submerged sections of pipeline transportation systems used in the petroleum, petrochemical and
natural gas industries as defined in ISO 13623. This document specifies the qualification, application and
testing of the corrosion protection coatings applied to steel surfaces left bare after the joining of pipes and
fittings (components) by welding.
This document defines and codifies in Table 1 the different types of field joint coatings for pipelines.
This document does not address requirements for additional mechanical protection, for thermal insulation
or for joint infills of concrete weight-coated pipes.
NOTE Field joints of pipes and fittings coated in accordance with this document are considered suitable for
further protection by means of cathodic protection.
2 Normative references
The following documents are referred to in the text in such a way that some or all of their content constitutes
requirements of this document. For dated references, only the edition cited applies. For undated references,
the latest edition of the referenced document (including any amendments) applies.
ISO 34-1, Rubber, vulcanized or thermoplastic — Determination of tear strength — Part 1: Trouser, angle and
crescent test pieces
ISO 37, Rubber, vulcanized or thermoplastic — Determination of tensile stress-strain properties
ISO 48-4, Rubber, vulcanized or thermoplastic — Determination of hardness — Part 4: Indentation hardness by
durometer method (Shore hardness)
ISO 188, Rubber, vulcanized or thermoplastic — Accelerated ageing and heat resistance tests
ISO 527-1, Plastics — Determination of tensile properties — Part 1: General principles
ISO 527-2, Plastics — Determination of tensile properties — Part 2: Test conditions for moulding and extrusion
plastics
ISO 527-3, Plastics — Determination of tensile properties — Part 3: Test conditions for films and sheets
ISO 868, Plastics and ebonite — Determination of indentation hardness by means of a durometer (Shore
hardness)
ISO 1431-1, Rubber, vulcanized or thermoplastic — Resistance to ozone cracking — Part 1: Static and dynamic
strain testing
ISO 1817, Rubber, vulcanized or thermoplastic — Determination of the effect of liquids
ISO/FDIS 21809-3:2026(en)
ISO 2178, Non-magnetic coatings on magnetic substrates — Measurement of coating thickness — Magnetic
method
ISO 2808, Paints and varnishes — Determination of film thickness
ISO 3303-1, Rubber- or plastics-coated fabrics — Determination of bursting strength — Part 1: Steel-ball method
ISO 4624, Paints and varnishes — Pull-off test for adhesion
ISO 6502-2, Rubber — Measurement of vulcanization characteristics using curemeters — Part 2: Oscillating
disc curemeter
ISO 5893, Rubber and plastics test equipment — Tensile, flexural and compression types (constant rate of
traverse) — Specification
ISO 8501-1, Preparation of steel substrates before application of paints and related products — Visual
assessment of surface cleanliness — Part 1: Rust grades and preparation grades of uncoated steel substrates and
of steel substrates after overall removal of previous coatings
ISO 8501-3, Preparation of steel substrates before application of paints and related products — Visual
assessment of surface cleanliness — Part 3: Preparation grades of welds, edges and other areas with surface
imperfections
ISO 8502-3, Preparation of steel substrates before application of paints and related products — Tests for the
assessment of surface cleanliness — Part 3: Assessment of dust on steel surfaces prepared for painting (pressure-
sensitive tape method)
ISO 8502-6, Preparation of steel substrates before application of paints and related products — Tests for
the assessment of surface cleanliness — Part 6: Extraction of water soluble contaminants for analysis (Bresle
method)
ISO 8502-9, Preparation of steel substrates before application of paints and related products — Tests for the
assessment of sur
...
ISO/FDIS 21809-3 :2026(en)
ISO/TC 67/SC 2
Secretariat: UNI
Date: 2026-06-0908-24
Oil and gas industries including lower carbon energy — External
coatings for buried or submerged pipelines used in pipeline
transportation systems — —
Part 3:
Field joint coatings
Industries du pétrole et du gaz, y compris les énergies à faible teneur en carbone — Revêtements externes des
conduites enterrées ou immergées utilisées dans les systèmes de transport par conduites —
Partie 3: Revêtements des joints réalisés sur site
FDIS stage
TTTTTThhhhhhiiiiiissssss d d d d d drrrrrraftaftaftaftaftaft i i i i i issssss s s s s s suuuuuubbbbbbmmmmmmiiiiiittttttttttttedededededed t t t t t toooooo a pa pa pa pa pa pararararararallel vallel vallel vallel vallel vallel vooooootttttte e e e e e iiiiiinnnnnn I I I I I ISSSSSSOOOOOO,,,,,, C C C C C CEEEEEENNNNNN.
ISO/FDIS 21809-3:2026(en)
All rights reserved. Unless otherwise specified, or required in the context of its implementation, no part of this publication
may be reproduced or utilized otherwise in any form or by any means, electronic or mechanical, including photocopying,
or posting on the internet or an intranet, without prior written permission. Permission can be requested from either ISO
at the address below or ISO’s member body in the country of the requester.
ISO copyright office
CP 401 • Ch. de Blandonnet 8
CH-1214 Vernier, Geneva
Phone: + 41 22 749 01 11
EmailE-mail: copyright@iso.org
Website: www.iso.org
Published in Switzerland
ii
ISO/FDIS 21809-3:2026(en)
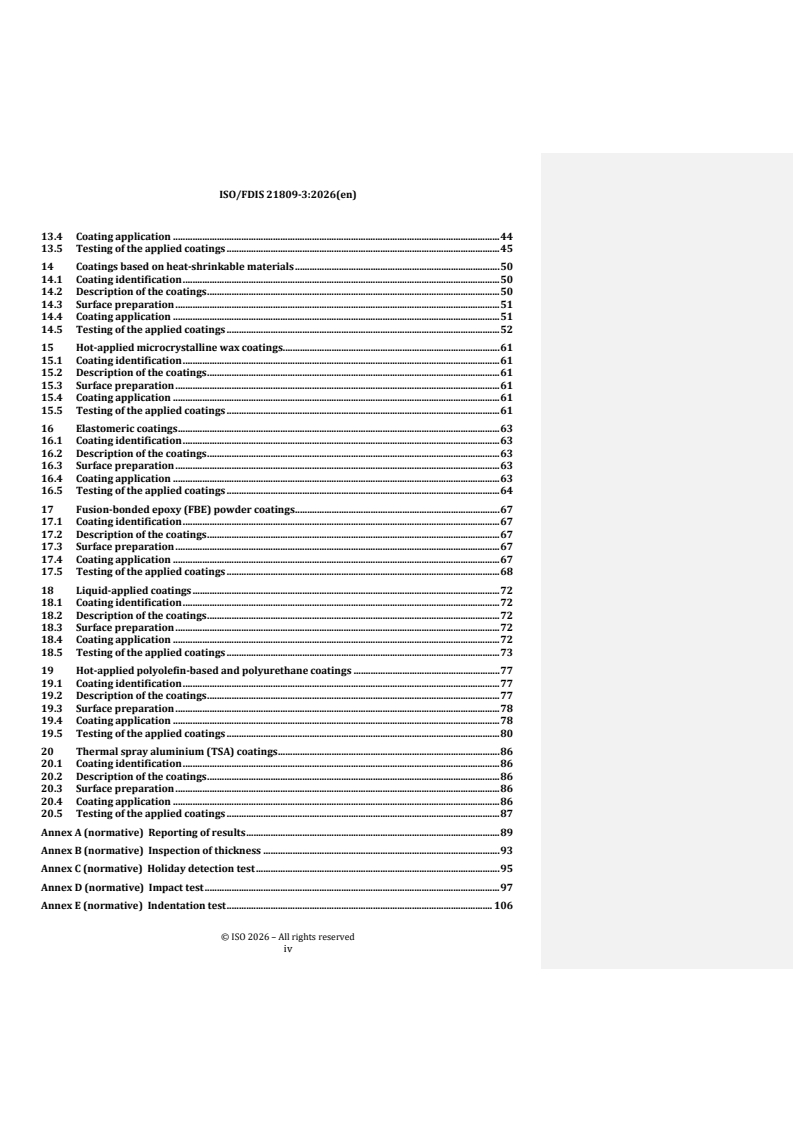
Contents
Foreword . vi
1 Scope . 1
2 Normative references . 1
3 Terms and definitions . 4
4 Symbols and abbreviated terms . 7
4.1 Symbols . 7
4.2 Abbreviated terms . 8
5 General requirements . 9
5.1 Responsibility of the end user . 9
5.2 Rounding . 9
5.3 Conformity, testing and quality . 9
6 Information to be supplied . 9
6.1 General. 9
6.2 Information to be supplied by the purchaser to the applicator. 9
6.3 Information to be supplied by the applicator to the purchaser. 10
7 Classification of field joint coatings. 11
8 Qualification processes . 12
8.1 Qualification of a coating system . 12
8.2 Coating application documents . 18
8.3 Qualification of coating operatives and inspection personnel . 24
9 Surface preparation . 26
9.1 General. 26
9.2 Preparation of the steel substrate . 29
9.3 Preparation of the adjacent plant coating . 31
10 Hot-applied bituminous tape coatings . 31
10.1 Coating identification . 31
10.2 Description of the coatings . 31
10.3 Surface preparation . 31
10.4 Coating application . 31
10.5 Testing of the applied coatings . 32
11 Petrolatum and wax-based tape coatings . 33
11.1 Coating identification . 33
11.2 Description of the coatings . 33
11.3 Surface preparation . 34
11.4 Coating application . 34
11.5 Testing of the applied coatings . 34
12 Cold-applied polymeric tape coatings . 38
12.1 Coating identification . 38
12.2 Description of the coatings . 38
12.3 Surface preparation . 38
12.4 Coating application . 38
12.5 Testing of the applied coatings . 39
13 Non-crystalline low-viscosity polyolefin-based coatings . 44
13.1 Coating identification . 44
13.2 Description of the coatings . 44
13.3 Surface preparation . 44
iii
ISO/FDIS 21809-3:2026(en)
13.4 Coating application . 44
13.5 Testing of the applied coatings . 45
14 Coatings based on heat-shrinkable materials . 50
14.1 Coating identification . 50
14.2 Description of the coatings . 50
14.3 Surface preparation . 51
14.4 Coating application . 51
14.5 Testing of the applied coatings . 52
15 Hot-applied microcrystalline wax coatings . 61
15.1 Coating identification . 61
15.2 Description of the coatings . 61
15.3 Surface preparation . 61
15.4 Coating application . 61
15.5 Testing of the applied coatings . 61
16 Elastomeric coatings . 63
16.1 Coating identification . 63
16.2 Description of the coatings . 63
16.3 Surface preparation . 63
16.4 Coating application . 63
16.5 Testing of the applied coatings . 64
17 Fusion-bonded epoxy (FBE) powder coatings . 67
17.1 Coating identification . 67
17.2 Description of the coatings . 67
17.3 Surface preparation . 67
17.4 Coating application . 67
17.5 Testing of the applied coatings . 68
18 Liquid-applied coatings . 72
18.1 Coating identification . 72
18.2 Description of the coatings . 72
18.3 Surface preparation . 72
18.4 Coating application . 72
18.5 Testing of the applied coatings . 73
19 Hot-applied polyolefin-based and polyurethane coatings . 77
19.1 Coating identification . 77
19.2 Description of the coatings . 77
19.3 Surface preparation . 78
19.4 Coating application . 78
19.5 Testing of the applied coatings . 80
20 Thermal spray aluminium (TSA) coatings . 86
20.1 Coating identification . 86
20.2 Description of the coatings . 86
20.3 Surface preparation . 86
20.4 Coating application . 86
20.5 Testing of the applied coatings . 87
Annex A (normative) Reporting of results . 89
Annex B (normative) Inspection of thickness . 93
Annex C (normative) Holiday detection test . 95
Annex D (normative) Impact test . 97
Annex E (normative) Indentation test . 106
iv
ISO/FDIS 21809-3:2026(en)
Annex F (normative) Specific electrical insulation resistance test . 109
Annex G (normative) Cathodic disbondment test . 121
Annex H (normative) Adhesion test (peel, lift and pull off). 140
Annex I (normative) Hot water immersion test . 155
Annex J (normative) Lap shear test . 158
Annex K (normative) Drip resistance test . 162
Annex L (normative) Peel strength between layers . 163
Annex M (normative) Thermal ageing resistance . 167
Annex N (normative) Coating porosity test . 172
Annex O (normative) Bursting strength of reinforced backing . 175
Annex P (normative) Thermal analysis of epoxy powder and cured coating film (FBE) . 176
Annex Q (normative) Adhesion test (X cut) — Resistance to removal . 185
Annex R (normative) Coating flexibility test . 188
Bibliography . 197
v
ISO/FDIS 21809-3:2026(en)
Foreword
ISO (the International Organization for Standardization) is a worldwide federation of national standards
bodies (ISO member bodies). The work of preparing International Standards is normally carried out through
ISO technical committees. Each member body interested in a subject for which a technical committee has been
established has the right to be represented on that committee. International organizations, governmental and
non-governmental, in liaison with ISO, also take part in the work. ISO collaborates closely with the
International Electrotechnical Commission (IEC) on all matters of electrotechnical standardization.
The procedures used to develop this document and those intended for its further maintenance are described
in the ISO/IEC Directives, Part 1. In particular, the different approval criteria needed for the different types of
ISO documentsdocument should be noted. This document was drafted in accordance with the editorial rules
of the ISO/IEC Directives, Part 2 (see www.iso.org/directives).
ISO draws attention to the possibility that the implementation of this document may involve the use of (a)
patent(s). ISO takes no position concerning the evidence, validity or applicability of any claimed patent rights
in respect thereof. As of the date of publication of this document, ISO had not received notice of (a) patent(s)
which may be required to implement this document. However, implementers are cautioned that this may not
represent the latest information, which may be obtained from the patent database available at
www.iso.org/patents. ISO shall not be held responsible for identifying any or all such patent rights.
Any trade name used in this document is information given for the convenience of users and does not
constitute an endorsement.
For an explanation of the voluntary nature of standards, the meaning of ISO specific terms and expressions
related to conformity assessment, as well as information about ISO's adherence to the World Trade
Organization (WTO) principles in the Technical Barriers to Trade (TBT), see www.iso.org/iso/foreword.html.
This document was prepared by Technical Committee ISO/TC 67, Oil and gas industries including lower carbon
energy, Subcommittee SC 2, Pipeline transportation systems., in collaboration with the European Committee
for Standardization (CEN) Technical Committee CEN/TC 12, Oil and gas industries including lower carbon
energy, in accordance with the Agreement on technical cooperation between ISO and CEN (Vienna
Agreement).
This third edition cancels and replaces the second edition (ISO 21809-3:2016), which has been technically
revised. It also incorporates the Amendment ISO 21809--3:2016/Amd 1:2020.
The main changes are as follows:
— inclusion of a qualification scheme;
— inclusion of new FJC types;
— changes in various FJC clauses;
— inclusion of new annexes;
— changes in various annexes.
A list of all parts in the ISO 21809 series can be found on the ISO website.
Any feedback or questions on this document should be directed to the user’s national standards body. A
complete listing of these bodies can be found at www.iso.org/members.html.
vi
ISO/FDIS 21809-3:2026(en)
Oil and gas industries including lower carbon energy — External
coatings for buried or submerged pipelines used in pipeline
transportation systems — —
Part 3:
Field joint coatings
1 Scope
This document specifies requirements for field joint coatings of seamless or welded steel pipes for buried and
submerged sections of pipeline transportation systems used in the petroleum, petrochemical and natural gas
industries as defined in ISO 13623. This document specifies the qualification, application and testing of the
corrosion protection coatings applied to steel surfaces left bare after the joining of pipes and fittings
(components) by welding.
This document defines and codifies in Table 1Table 1 the different types of field joint coatings for pipelines.
This document does not address requirements for additional mechanical protection, for thermal insulation or
for joint infills of concrete weight-coated pipes.
NOTE Field joints of pipes and fittings coated in accordance with this document are considered suitable for further
protection by means of cathodic protection.
2 Normative references
The following documents are referred to in the text in such a way that some or all of their content constitutes
requirements of this document. For dated references, only the edition cited applies. For undated references,
the latest edition of the referenced document (including any amendments) applies.
ISO 34--1, Rubber, vulcanized or thermoplastic — Determination of tear strength — Part 1: Trouser, angle and
crescent test pieces
ISO 37, Rubber, vulcanized or thermoplastic — Determination of tensile stress-strain properties
ISO 48-4, Rubber, vulcanized or thermoplastic — Determination of hardness — Part 4: Indentation hardness by
durometer method (Shore hardness)
ISO 188, Rubber, vulcanized or thermoplastic — Accelerated ageing and heat resistance tests
ISO 527--1, Plastics — Determination of tensile properties — Part 1: General principles
ISO 527--2, Plastics — Determination of tensile properties — Part 2: Test conditions for moulding and extrusion
plastics
ISO 527--3, Plastics — Determination of tensile properties — Part 3: Test conditions for films and sheets
ISO 868, Plastics and ebonite — Determination of indentation hardness by means of a durometer (Shore
hardness)
ISO 1431--1, Rubber, vulcanized or thermoplastic — Resistance to ozone cracking — Part 1: Static and dynamic
strain testing
ISO/FDIS 21809-3:2026(en)
ISO 1817, Rubber, vulcanized or thermoplastic — Determination of the effect of liquids
ISO 2178, Non-magnetic coatings on magnetic substrates — Measurement of coating thickness — Magnetic
method
ISO 2808, Paints and varnishes — Determination of film thickness
ISO 3183, Petroleum and natural gas industries — Steel pipe for pipeline transportation systems
ISO 3303--1, Rubber- or plastics-coated fabrics — Determination of bursting strength — Part 1: Steel-ball
method
ISO 3417, Rubber — Measurement of vulcanization characteristics with the oscillating disc curemeter
ISO 4624, Paints and varnishes — Pull-off test for adhesion
ISO 6502-2, Rubber — Measurement of vulcanization characteristics using curemeters — Part 2: Oscillating disc
curemeter
ISO 5893, Rubber and plastics test equipment — Tensile, flexural and compression types (constant rate of
traverse) — Specification
ISO 7619-1, Rubber, vulcanized or thermoplastic — Determination of indentation hardness — Part 1:
Durometer method (Shore hardness)
ISO 8501--1, Preparation of steel substrates before application of paints and related products — Visual
assessment of surface cleanliness — Part 1: Rust grades and preparation grades of uncoated steel substrates and
of steel substrates after overall removal of previous coatings
ISO 8501--3, Preparation of steel substrates before application of paints and related products — Visual
assessment of surface cleanliness — Part 3: Preparation grades of welds, edges and other areas with surface
imperfections
ISO 8502--3, Preparation of steel substrates before application of paints and related products — Tests for the
assessment of surface cleanliness — Part 3: Assessment of dust on steel surfaces prepared for painting (pressure-
sensitive tape method)
ISO 8502--6, Preparation of steel substrates before application of paints and related products — Tests for the
assessment of surface cleanliness — Part 6: Extraction of water soluble contaminants for analysis (Bresle
method)
ISO 8502--9, Preparation of steel substrates before application of paints and related products — Tests for the
assessment of surface cleanliness — Part 9: Field method for the conductometric determination of water-soluble
salts
ISO 8503--4, Preparation of steel substrates before application of paints and related products — Surface
roughness characteristics of blast-cleaned steel substrates — Part 4: Method for the calibration of ISO surface
profile comparators and for the determination of surface profile — Stylus instrument procedure
ISO 8503--5, Preparation of steel substrates before application of paints and related products — Surface
roughness characteristics of blast-cleaned steel substrates — Part 5: Replica tape method for the determination
of the surface profile
ISO 8504--2, Preparation of steel substrates before application of paints and related products — Surface
preparation methods — Part 2: Abrasive blast-cleaning
ISO/FDIS 21809-3:2026(en)
ISO 8504--3, Preparation of steel substrates before application of paints and related products — Surface
preparation methods — Part 3: Hand- and power-tool cleaning
ISO 10474, Steel and steel products — Inspection documents
ISO 11124 (all parts), Preparation of steel substrates before application of paints and related products —
Specifications for metallic blast-cleaning abrasives
ISO 11125 (all parts), Preparation of steel substrates before application of paints and related products — Test
methods for metallic blast-cleaning abrasives
ISO 11126 (all parts), Preparation of steel substrates before application of paints and related products —
Specifications for non-metallic blast-cleaning abrasives
ISO 11127 (all parts), Preparation of steel substrates before application of paints and related products — Test
methods for non-metallic blast-cleaning abrasives
ISO 11357--1, Plastics — Differential scanning calorimetry (DSC) — Part 1: General principles
ISO 11357--2, Plastics — Differential scanning calorimetry (DSC) — Part 2: Determination of glass transition
temperature and step height
ISO 11357--3, Plastics — Differential scanning calorimetry (DSC) — Part 3: Determination of temperature and
enthalpy of melting and crystallization
ISO 11357--6, Plastics — Differential scanning calorimetry (DSC) — Part 6: Determination of oxidation
induction time (isothermal OIT) and oxidation induction temperature (dynamic OIT)
ISO 13623, Petroleum and natural gas industries — Pipeline transportation systems
ISO/IEC 17025, General requirements for the competence of testing and calibration laboratories
ISO 80000--1:2022, Quantities and units — Part 1: General
EN 10204, Metallic products — Types of inspection documents
1)
ASTM D70, , Standard Test Method for Density of Semi-Solid Bituminous Materials (Pycnometer Method)
ASTM D92, Standard Test Method for Flash and Fire Points by Cleveland Open Cup Tester
ASTM D127, Standard Test Method for Drop Melting Point of Petroleum Wax, Including Petrolatum
ASTM D149, Standard Test Method for Dielectric Breakdown Voltage and Dielectric Strength of Solid Electrical
Insulating Materials at Commercial Power Frequencies
ASTM D1141, Standard Practice for the Preparation of Substitute Ocean Water
ASTM D1321, Standard Test Method for Needle Penetration of Petroleum Waxes
ASTM D2084, Standard Test Method for Rubber Property — Vulcanization Using Oscillating Disk Cure Meter
ASTM D4285, Standard Test Method for Indicating Oil or Water in Compressed Air
1)
American Society for Testing and Materials, 100 Harbour Drive, West Conshohocken, PA 19428-2959, USA.
ISO/FDIS 21809-3:2026(en)
ASTM D4940, Standard Test Method for Conductimetric Analysis of Water Soluble Ionic Contamination of Blast
Cleaning Abrasives
2)
AWS C2.25/C2.25M, , Specification for Thermal Spray Feedstock Solid and Composite Wire and Ceramic Rods
3)
SSPC-SP1, , Surface preparation specification (NACE No.1) — Solvent cleaning
SSPC Guide 15, Field Methods for Extraction and Analysis of Soluble Salts on Steel and Other Nonporous
Substrates
SSPC CS 23.00, Specification for the Application of Thermal Spray Coatings (Metallizing) of Aluminium, Zinc and
Their Alloys and Composites for the Corrosion Protection of Steel
3 Terms and definitions
For the purposes of this document, the following terms and definitions apply.
ISO and IEC maintain terminology databases for use in standardization at the following addresses:
— — ISO Online browsing platform: available at https://www.iso.org/obp
— — IEC Electropedia: available at https://www.electropedia.org/
3.1 3.1
additional mechanical protection
various materials to either enhance impact and indentation resistance or isolate movements between field
joint coating and surrounding soil, or both
Note 1 to entry: This includes additional layer(s) partially or not bonded over the specified anti-corrosion system
qualified by this standard. The additional mechanical layer(s) shall be compatible with cathodic protection so as to not
prevent current reaching and protecting the pipe. The properties, components, and application methods of those
additional layers are not covered by this standard.
3.2 3.2
application procedure specification
APS
document describing procedures, methods, equipment and tools used for field joint coating application
3.3 3.3
applicator
company that undertakes the coating application in accordance with the provisions of this document
Note 1 to entry: If the compounding of the top layer is done prior or during the application process by the applicator,
then the applicator is regarded as the manufacturer (3.19(3.19).).
3.4 3.4
batch
quantity of material produced in a continuous manufacturing operation using raw materials of the same
source and grade
2)
America Welding Society, 550 N.W. Le Jeune Road, Miami, Florida 33126, USA.
3) th th
The Society for Protective Coatings, 40 24 Street, 6 Floor, Pittsburgh, PA 15222-4656, USA.
ISO/FDIS 21809-3:2026(en)
3.5 3.5
batch certificate
certificate of analysis (3.9(3.9)) issued by the manufacturer (3.19(3.19)) for a given batch (3.4(3.4)) of each
coating system component
3.6 3.6
bonding agent
material applied as a film to the primed substrate in order to ensure adhesion of the subsequent protective
coating
3.7 3.7
coating operative
individual undertaking coating activity on the work site, including surface preparation
3.8 3.8
coating system
single or multiple layers of coating material applied to a metal surface for protection against corrosion by
preventing contact between the electrolyte and the metal surface
3.9 3.9
certificate of analysis
document provided by the manufacturer (3.19(3.19)) which indicates results of specific tests or analysis,
including test methodology, performed on a defined lot of the manufacturer’s product and corresponding
conformity ranges
3.10 3.10
cutback
length of pipe left uncoated at each end for joining purposes (e.g. welding)
3.11 3.11
design temperature range
temperature range, including maximum and minimum temperatures, likely to be reached during transport,
storage, handling, installation and operation
Note 1 to entry: The design temperature range of the field joint coating can be narrower than that specified for the steel
pipe material or the pipeline system (3.25(3.25),), or both.
3.12 3.12
end user
company that owns or operates the pipeline system (3.25(3.25),), or both
3.13 3.13
field joint area
uncoated area that results when two pipe sections or a pipe section and a fitting with coating cutbacks
(3.10(3.10)) are assembled by welding in the field
3.14 3.14
holiday
coating discontinuity that exhibits electrical conductivity when exposed to a specific voltage
3.15 3.15
inspection document
document stating conformity with the requirements given in the purchase order
ISO/FDIS 21809-3:2026(en)
Note 1 to entry: The inspection document shall be issued in accordance with ISO 10474 (or EN 10204).
3.16 3.16
inspection and testing plan
ITP
document providing an overview of the sequence of inspections and tests, including resources and procedures
references
3.17 3.17
inspector
representative responsible for one or more of the inspections specified in this document
3.18 3.18
layer of tape
single wrap of tape without overlap
Note 1 to entry: Wrapping of a tape with 50 % overlap constitutes a two-layer tape coating.
3.19 3.19
manufacturer
company responsible for the manufacture of coating material(s)
3.20 3.20
maximum service temperature
T
max
maximum continuous temperature that the field joint coating can resist
3.21 3.21
nominal thickness
numerical designation of the thickness exclusive of tolerances, allowances etc. of supplied materials
3.22 3.22
operating temperature
temperature that can be endured by a pipeline (component) or pipeline system (3.25(3.26)) during operation,
within the design temperature range (3.11(3.11),), or both
3.23 3.23
party
stakeholder ([end user, purchaser (3.29(3.29),), applicator (3.3(3.3),), manufacturer (3.19(3.19),), etc.).] with
a vested interest in the decision-making
3.24 3.24
pipeline
facilities through which fluids are conveyed, including pipe, pig traps, components and appurtenances, up to
and including the isolating valves
[SOURCE: ISO 13623:2017, 3.1.1615]
3.25 3.25
pipeline system
pipelines (3.24(3.25),), stations, supervisory control and data acquisition system (SCADA), safety systems,
corrosion protection systems, and any other equipment, facility or building used in the transportation of fluids
[SOURCE: ISO 13623:2017, 3.1.16]
ISO/FDIS 21809-3:2026(en)
3.26 3.26
pre-production trial
PPT
application of coating and inspection or testing of its properties immediately prior to start of production, to
confirm that field joint coatings produced in accordance with the APS (3.2(3.2)) and ITP (3.16(3.16)) are
acceptable within the specified properties
3.27 3.27
primer
material applied as a film on substrate to ensure adhesion of the subsequent protective coating
3.28 3.28
procedure qualification trial
PQT
application of a field joint coating and subsequent inspection or testing of its properties, to confirm that field
joint coatings produced in accordance with the APS (3.2(3.2)) and ITP (3.16(3.16)) are acceptable within the
specified properties, carried out at the premises of the applicator (3.3(3.3)) or any other agreed location
3.29 3.29
purchaser
company responsible for providing the purchase order requirements.
3.30 3.30
shift
time period during which a crew of workers is at work
3.31 3.31
test sample
sample from a batch (3.4(3.4)) of raw material or field joint coating that represents the properties of the
complete batch
3.32 3.32
test specimen
object prepared for the purpose of testing specific properties
Note 1 to entry: The test specimens can be as follows: the coating material; a simulated field joint, flat panel
or similar prepared specifically for testing; a coupon, ring or similar that has been cut from a field joint; a field
joint that has been coated in production or otherwise, in laboratory or field conditions.
3.33 3.33
wrap-around sleeve
sleeve wrapped circumferentially around the steel pipe area being coated
4 Symbols and abbreviated terms
4.1 Symbols
B bursting strength after thermal ageing for 70 days
B100 bursting strength after thermal ageing for 100 days
C percentage of conversion of FBE coating
ΔH exothermic heat of reaction
ΔTg variation of glass transition temperature between two or more successive thermal analysis scans
ISO/FDIS 21809-3:2026(en)
E0 elongation at break without thermal ageing
E elongation at break after thermal ageing for 14 days
E elongation at break after thermal ageing for 70 days
E elongation at break after thermal ageing for 100 days
P28 peel strength to pipe surface after thermal ageing or hot water immersion for 28 days
P peel strength to pipe surface after thermal ageing for 70 days
P peel strength to pipe surface after thermal ageing or hot water immersion for 100 days
Pt Minimum peel strength to surface or plant coating as specified in the table of FJC requirements
P′ peel strength between layers after thermal ageing or hot water immersion for 70 days
P′ peel strength between layers after thermal ageing or hot water immersion for 100 days
P’ Minimum peel strength between layers as specified in the table of FJC requirements
t
RS specific electrical insulation resistance of a coating
R specific electrical insulation resistance after 70 days
S70
R specific electrical insulation resistance after 100 days
S100
T glass transition temperature
g
4.2 Abbreviated terms
CQ coating qualification
CSQ coating system qualification
DFT dry film thickness
DSC differential scanning calorimetry
EP epoxy
EPDM ethylene propylene diene monomer
FBE fusion-bonded epoxy
FJC field joint coating
HSS heat-shrink sleeve
SDS safety data sheet
PE polyethylene
PDS product data sheet
PP polypropylene
PU polyurethane
PVC polyvinylchloride
TSA thermal spray aluminium
2LPE two-layer polyethylene coating
3LPE three-layer polyethylene coating
3LPP three-layer polypropylene coating
ISO/FDIS 21809-3:2026(en)
5 General requirements
5.1 Responsibility of the end user
The end user shall be responsible for making or approving the appropriate selection of the FJC in accordance
with the specified service, coating application and installation conditions. The end user shall validate the
information to be supplied by the purchaser as listed in Clause 6Clause 6.
5.2 Rounding
Unless otherwise stated in this document, to determine conformity with the specified requirements, observed
or calculated values shall be rounded to the nearest unit in the last right-hand place of figures used in
expressing the limiting value, in accordance with ISO 80000--1:2022, Annex B, Rule B.
NOTE For the purposes of this provision, the rounding method of ASTM E29 is equivalent to ISO 80000--1:2022,
Annex B, Rule B.
5.3 Conformity, testing and quality
Systems for quality and environmental management, and good laboratory practices, should be applied to
assist conformity with the requirements of this document.
Test reports shall be in accordance with Annex A, unless otherwise specified.
NOTE 1 ISO 29001 gives sector-specific guidance on quality management systems.
NOTE 2 ISO 14001 gives guidance on the selection and use of an environmental management system.
6 Information to be supplied
6.1 General
CQ, CSQ, PQT, PPT, APS and ITP are described in Clause 8Clause 8.
6.2 Information to be supplied by the purchaser to the applicator
The purchaser shall provide the following information:
— — designation of this document to the relevant field joint coating system in accordance with
Table 1Table 1;;
— — CSQ requirements;
— — project requirements:
— — brand and type of FJC system (if applicable);
— — applicable project specifications;
— — PQT and / or PPT requirements (if applicable);
— — pipe material or grade (e.g. ISO 3183);
— — pipe nominal outer diameter and wall thickness;
— — design temperature range and operating temperature of the pipeline (if relevant);
ISO/FDIS 21809-3:2026(en)
— — minimum and maximum thickness of the field joint coating (if applicable);
— — chamfer or cutback design (size, length or geometry of the field joint being coated), including
tolerances for both ends of pipe or fittings (if relevant), or both;
— — plant coating system including minimum or maximum thickness;
— — overlap on the parent (i.e. “plant-applied”) coating or detailed drawing of the field joint coating
with dimensional tolerances (if relevant);
— — maximum permissible preheating temperature;
— — expected environmental temperature range during field joint coating application;
— — water depth (if applicable);
— — soil properties (if applicable);
— — expected temperature range during pipeline installation;
— — method of installation of the pipeline;
— — number of field joints to be coated;
— — permissible number and size of field joint and plant coating repairs;
— — time constraints for application and number and dimensions of working stations, if relevant;
— — restrictions in field joint coating application caused by the design of fittings (if applicable);
— — restrictions in accessibility, available space, environmental conditions and other at coating
application location (if applicable);
— — special requirements for handling and storage procedures (if applicable);
— — required qualification of the applicator's personnel performing surface preparation or coating
application, or both and personnel performing inspection of surface preparation or coating application, or
both;
— — requested schedule of delivery of coating systems;
— — requested documentation and schedule for supply of documentation;
— — requirements on test reports and (daily) log;
— — type and frequency of inspection document in accordance with ISO 10474 or EN 10204 (see
8.2.38.2.3););
— — requirements for traceability of field joint coating systems or repair systems and marking.
6.3 Information to be supplied by the applicator to the purchaser
The applicator shall provide the following information, if relevant, based on information from the coating
(materi
...
PROJET FINAL
Norme
internationale
ISO/FDIS 21809-3
ISO/TC 67/SC 2
Industries du pétrole et du gaz,
Secrétariat: UNI
y compris les énergies à faible
Début de vote:
teneur en carbone — Revêtements
2026-09-21
externes des conduites enterrées
Vote clos le:
ou immergées utilisées dans
2026-11-16
les systèmes de transport par
conduites —
Partie 3:
Revêtements des joints soudés sur
site
Oil and gas industries including lower carbon energy — External
coatings for buried or submerged pipelines used in pipeline
transportation systems —
Part 3: Field joint coatings
LES DESTINATAIRES DU PRÉSENT PROJET SONT
INVITÉS À PRÉSENTER, AVEC LEURS OBSERVATIONS,
NOTIFICATION DES DROITS DE PROPRIÉTÉ DONT ILS
AURAIENT ÉVENTUELLEMENT CONNAISSANCE ET À
FOURNIR UNE DOCUMENTATION EXPLICATIVE.
OUTRE LE FAIT D’ÊTRE EXAMINÉS POUR
ÉTABLIR S’ILS SONT ACCEPTABLES À DES FINS
INDUSTRIELLES, TECHNOLOGIQUES ET COM-MERCIALES,
AINSI QUE DU POINT DE VUE DES UTILISATEURS, LES
PROJETS DE NORMES
TRAITEMENT PARALLÈLE ISO/CEN
INTERNATIONALES DOIVENT PARFOIS ÊTRE CONSIDÉRÉS
DU POINT DE VUE DE LEUR POSSI BILITÉ DE DEVENIR DES
NORMES POUVANT
SERVIR DE RÉFÉRENCE DANS LA RÉGLEMENTATION
NATIONALE.
Numéro de référence
ISO/FDIS 21809-3:2026(fr) © ISO 2026
PROJET FINAL
ISO/FDIS 21809-3:2026(fr)
Norme
internationale
ISO/FDIS 21809-3
ISO/TC 67/SC 2
Industries du pétrole et du gaz,
Secrétariat: UNI
y compris les énergies à faible
Début de vote:
teneur en carbone — Revêtements
2026-09-21
externes des conduites enterrées
Vote clos le:
ou immergées utilisées dans
2026-11-16
les systèmes de transport par
conduites —
Partie 3:
Revêtements des joints soudés sur
site
Oil and gas industries including lower carbon energy — External
coatings for buried or submerged pipelines used in pipeline
transportation systems —
Part 3: Field joint coatings
DOCUMENT PROTÉGÉ PAR COPYRIGHT
© ISO 2026
LES DESTINATAIRES DU PRÉSENT PROJET SONT
Tous droits réservés.
INVITÉS À PRÉSENTER, AVEC LEURS OBSERVATIONS,
NOTIFICATION DES DROITS DE PROPRIÉTÉ DONT ILS
La présente publication de l’ISO est protégée par le droit d’auteur et demeure la propriété de l’ISO et/ou de ses concédants de
AURAIENT ÉVENTUELLEMENT CONNAISSANCE ET À
licence.
FOURNIR UNE DOCUMENTATION EXPLICATIVE.
Le contenu de la présente publication de l’ISO est fourni sous licence, et n’est pas vendu. Son utilisation est soumise aux conditions
OUTRE LE FAIT D’ÊTRE EXAMINÉS POUR
ÉTABLIR S’ILS SONT ACCEPTABLES À DES FINS
de licence applicables définies par l’ISO, un organisme membre de l’ISO, ou un distributeur tiers agréé.
INDUSTRIELLES, TECHNOLOGIQUES ET COM-MERCIALES,
Sous réserve des besoins liés à sa mise en œuvre ou d’une autorisation expresse prévue aux termes d’une licence distincte, aucune
AINSI QUE DU POINT DE VUE DES UTILISATEURS, LES
partie de la présente publication de l’ISO ne peut être reproduite, distribuée, modifiée, utilisée ou mise à disposition sous quelque PROJETS DE NORMES
TRAITEMENT PARALLÈLE ISO/CEN
INTERNATIONALES DOIVENT PARFOIS ÊTRE CONSIDÉRÉS
forme ou par quelque moyen que ce soit – électronique ou mécanique, y compris la photocopie, la numérisation, l’enregistrement
DU POINT DE VUE DE LEUR POSSI BILITÉ DE DEVENIR DES
ou la publication sur des plateformes numériques internes ou externes.
NORMES POUVANT
SERVIR DE RÉFÉRENCE DANS LA RÉGLEMENTATION
Toute utilisation hors du champ d’application des droits accordés est interdite et peut donner lieu à des poursuites judiciaires.
NATIONALE.
ISO copyright office
Case postale 401 • CH-1214 Vernier, Genève
Tél.: +41 22 749 01 11
E-mail: copyright@iso.org
Web: www.iso.org
Publié en Suisse
Numéro de référence
ISO/FDIS 21809-3:2026(fr) © ISO 2026
ii
ISO/FDIS 21809-3:2026(fr)
Sommaire Page
Avant-propos .vii
1 Domaine d'application . 1
2 Références normatives . 1
3 Termes et définitions . 3
4 Symboles et abréviations . 7
4.1 Symboles .7
4.2 Abréviations.8
5 Exigences générales . . 8
5.1 Responsabilités de l'utilisateur final .8
5.2 Arrondis.8
5.3 Conformité, essais et qualité .9
6 Informations à fournir . 9
6.1 Généralités .9
6.2 Informations à fournir par l'acheteur à l'applicateur .9
6.3 Informations à fournir par l'applicateur à l'acheteur .10
7 Classification des revêtements de joints soudés sur site.11
8 Processus de qualification .12
8.1 Qualification d'un système de revêtement . 12
8.1.1 Généralités . 12
8.1.2 Qualification du revêtement (CQ) à l'initiative du fabricant . 13
8.1.3 Essai de qualification du mode opératoire (PQT) à l'initiative de l'applicateur .14
8.1.4 Qualification du système de revêtement (CSQ) à l'initiative de l'applicateur . 15
8.1.5 Essai de pré-production (PPT) à l'initiative de l'applicateur .16
8.1.6 Inspection et essais pendant la production.16
8.2 Documents d'application du revêtement . .17
8.2.1 Spécification du mode opératoire d'application (APS) .17
8.2.2 Plan de contrôles et d'essais (ITP) . 20
8.2.3 Exigences et modes opératoires .21
8.2.4 Documents d'inspection, traçabilité et vérification . 22
8.3 Qualification des opérateurs de revêtement et du personnel du contrôle . 22
8.3.1 Généralités . 22
8.3.2 Qualification des opérateurs de revêtement . 23
8.3.3 Preuve documentaire de la qualification des opérateurs de revêtement de
l'Applicateur .24
8.3.4 Requalification .24
9 Préparation de surface . .25
9.1 Généralités . 25
9.2 Préparation du substrat en acier .27
9.2.1 Généralités .27
9.2.2 Décapage par projection d'abrasif . 28
9.2.3 Nettoyage à la brosse métallique . 28
9.2.4 Autres méthodes de nettoyage . 28
9.3 Préparation du revêtement d'usine adjacent . 28
10 Revêtements à base de bandes bitumineuses appliquées à chaud.29
10.1 Identification du revêtement . 29
10.2 Description des revêtements . 29
10.3 Préparation de surface . 29
10.4 Application du revêtement. 29
10.5 Essais des revêtements appliqués . 29
11 Revêtements en bande de pétrolatum et à base de cire .31
11.1 Identification du revêtement .31
iii
ISO/FDIS 21809-3:2026(fr)
11.2 Description des revêtements .32
11.2.1 Bandes de pétrolatum (Type 11A) .32
11.2.2 Bandes à base de cire (Type 11B) . .32
11.3 Préparation de surface .32
11.4 Application du revêtement.32
11.5 Essais des revêtements appliqués .32
12 Revêtements de bandes polymères appliquées à froid.36
12.1 Identification du revêtement . 36
12.2 Description des revêtements . 36
12.2.1 Revêtements de bandes appliquées à froid à support polymère continu
(Type 12A) . 36
12.2.2 Revêtements de bandes appliquées à froid à support polymère maillé (Type 12B) . 36
12.3 Préparation de surface . 36
12.4 Application du revêtement. 36
12.5 Essais des revêtements appliqués .37
13 Revêtements à base de polyoléfine non cristalline à faible viscosité .42
13.1 Identification du revêtement .42
13.2 Description des revêtements .42
13.3 Préparation de surface .42
13.4 Application du revêtement.42
13.5 Essais des revêtements appliqués .43
13.5.1 Généralités .43
13.5.2 Contrôle préalable à l'application d'un composé renforcé .43
14 Revêtements à base de matériaux thermorétractables .49
14.1 Identification du revêtement . 49
14.2 Description des revêtements . 49
14.2.1 Généralités . 49
14.2.2 Type 14A . 49
14.2.3 Types 14B, 14C et 14D . 49
14.3 Préparation de surface . 50
14.4 Application du revêtement. 50
14.5 Essais des revêtements appliqués . 50
15 Revêtements de cire microcristalline appliqués à chaud .58
15.1 Identification du revêtement . 58
15.2 Description des revêtements . 58
15.3 Préparation de surface . 58
15.4 Application du revêtement. 58
15.5 Essais des revêtements appliqués . 58
16 Revêtements élastomères .60
16.1 Identification du revêtement . 60
16.2 Description des revêtements . 60
16.3 Préparation de surface . 60
16.4 Application du revêtement. 60
16.4.1 Généralités . 60
16.4.2 Méthode de vulcanisation in situ . . 60
16.5 Essais des revêtements appliqués .61
16.5.1 Généralités .61
16.5.2 Courbe de rhéomètre — Disque oscillant . 64
16.5.3 Résistivité électrique volumique . 64
17 Revêtements à base de poudre époxyde appliquée par fusion (FBE) .64
17.1 Identification du revêtement . 64
17.2 Description des revêtements . 64
17.3 Préparation de surface . 64
17.4 Application du revêtement. 64
17.4.1 Généralités . 64
17.4.2 Transport et stockage de la poudre époxyde . 65
iv
ISO/FDIS 21809-3:2026(fr)
17.4.3 Chauffage . 65
17.4.4 Application de la poudre époxyde . 65
17.5 Essais des revêtements appliqués . 65
17.5.1 Généralités . 65
17.5.2 Épaisseur . 65
18 Revêtements appliqués sous forme liquide .69
18.1 Identification du revêtement . 69
18.2 Description des revêtements . 69
18.2.1 Époxyde liquide — 18A . 69
18.2.2 Polyuréthane liquide — 18B . 69
18.2.3 Époxyde renforcée de fibres — 18C . 69
18.2.4 Vinylester renforcé de fibres — 18D . 69
18.2.5 Polyuréthane renforcée de fibres — 18E . 69
18.2.6 Enveloppe de polyoléfine avec remplissage en polyuréthane — 18F . 69
18.3 Préparation de surface . 69
18.4 Application du revêtement. 69
18.4.1 Généralités . 69
18.4.2 Chauffage .70
18.4.3 Application des revêtements liquides.70
18.4.4 Lignes directrices générales .70
18.5 Essais des revêtements appliqués .70
19 Revêtements à base de polyoléfine et de polyuréthane appliqués à chaud . 74
19.1 Identification du revêtement .74
19.2 Description des revêtements .74
19.2.1 Revêtements à base de poudre de polypropylène dispersée dans la flamme,
appliqués sur une couche de résine époxyde — Type 19A .74
19.2.2 Revêtements à base de bandes/feuilles/profilés extrudés de polypropylène,
appliqués à chaud sur une couche de résine époxyde — Type 19B .74
19.2.3 Revêtements à base de polypropylène moulé par injection sur une couche de
résine époxyde — Type 19C .74
19.2.4 Revêtements à base de poudre de polyéthylène dispersée dans la flamme,
appliqués sur une couche de résine époxyde — Type 19D .74
19.2.5 Revêtements à base de bandes/feuilles/profilés extrudés de polyéthylène,
appliqués à chaud sur une couche de résine époxyde — Type 19E . 75
19.2.6 Revêtements à base de polyéthylène moulé par injection sur une couche de
résine époxyde — Type 19F. 75
19.2.7 Revêtements à base de polyuréthane moulé par injection sur une couche
primaire de résine époxyde ou de polyuréthane — Type 19G . 75
19.3 Préparation de surface . 75
19.4 Application du revêtement. 75
19.4.1 Généralités . 75
19.4.2 Chauffage .76
19.4.3 Application du primaire .76
19.4.4 Application du PP ou PE chimiquement modifié .76
19.4.5 Application de la couche de finition .76
19.5 Essais des revêtements appliqués . 77
20 Revêtements en aluminium projeté à chaud (TSA) .88
20.1 Identification du revêtement . 88
20.2 Description des revêtements . 88
20.3 Préparation de surface . 88
20.4 Application du revêtement. 88
20.4.1 Généralités . 88
20.4.2 Aluminium . 88
20.4.3 Bouche-pores . 89
20.5 Essais des revêtements appliqués . 89
Annexe A (normative) Compte-rendu des résultats .91
v
ISO/FDIS 21809-3:2026(fr)
Annexe B (normative) Contrôle de l'épaisseur .95
Annexe C (normative) Essai de détection des porosités .97
Annexe D (normative) Essai de résistance aux chocs .99
Annexe E (normative) Essai d'indentation .107
Annexe F (normative) Essai de résistance d'isolement électrique spécifique .110
Annexe G (normative) Essai de décollement cathodique .121
Annexe H (normative) Essai d'adhérence (pelage, soulèvement et traction) .136
Annexe I (normative) Essai d'immersion dans l'eau chaude .148
Annexe J (normative) Essai de cisaillement du recouvrement.151
Annexe K (normative) Essai de résistance à la formation de gouttes .155
Annexe L (normative) Résistance au pelage entre couches .156
Annexe M (normative) Résistance au vieillissement thermique .159
Annexe N (normative) Essai de porosité du revêtement . 164
Annexe O (normative) Résistance à l'éclatement du support renforcé .166
Annexe P (normative) Analyse thermique de la poudre époxydique et du film réticulé de
revêtement (FBE) .167
Annexe Q (normative) Essai d'adhérence (incision en X) — Résistance au retrait .174
Annexe R (normative) Essai de flexibilité du revêtement .176
Bibliographie .183
vi
ISO/FDIS 21809-3:2026(fr)
Avant-propos
L'ISO (Organisation internationale de normalisation) est une fédération mondiale d'organismes nationaux
de normalisation (comités membres de l'ISO). L'élaboration des Normes internationales est en général
confiée aux comités techniques de l'ISO. Chaque comité membre intéressé par une étude a le droit de faire
partie du comité technique créé à cet effet. Les organisations internationales, gouvernementales et non
gouvernementales, en liaison avec l'ISO participent également aux travaux. L'ISO collabore étroitement avec
la Commission électrotechnique internationale (IEC) en ce qui concerne la normalisation électrotechnique.
Les procédures utilisées pour élaborer le présent document et celles destinées à sa mise à jour sont
décrites dans les Directives ISO/IEC, Partie 1. Il convient, en particulier, de prendre note des différents
critères d'approbation requis pour les différents types de documents ISO. Le présent document
a été rédigé conformément aux règles de rédaction données dans les Directives ISO/IEC, Partie 2
(voir www.iso.org/directives).
L'ISO attire l'attention sur le fait que la mise en application du présent document peut entraîner l'utilisation
d'un ou de plusieurs brevets. L'ISO ne prend pas position quant à la preuve, à la validité et à l'applicabilité de
tout droit de propriété revendiqué à cet égard. À la date de publication du présent document, l'ISO n'avait pas
reçu notification qu'un ou plusieurs brevets pouvaient être nécessaires à sa mise en application. Toutefois,
il y a lieu d'avertir les responsables de la mise en application du présent document que des informations
plus récentes sont susceptibles de figurer dans la base de données de brevets, disponible à l'adresse
www.iso.org/brevets. L'ISO ne saurait être tenue pour responsable de ne pas avoir identifié de tels droits de
propriété et averti de leur existence.
Les appellations commerciales éventuellement mentionnées dans le présent document sont données pour
information, par souci de commodité, à l'intention des utilisateurs et ne sauraient constituer un engagement.
Pour une explication de la nature volontaire des normes, la signification des termes et expressions
spécifiques de l'ISO liés à l'évaluation de la conformité, ou pour toute information au sujet de l'adhésion de
l'ISO aux principes de l'Organisation mondiale du commerce (OMC) concernant les obstacles techniques au
commerce (OTC), voir www.iso.org/avant-propos.
Le présent document a été élaboré par le comité technique ISO/TC 67, Industries du pétrole et du gaz, y compris
les énergies à faible teneur en carbone, sous-comité SC 2, Systèmes de transport par conduites, en collaboration
avec le comité technique CEN/TC 12, Industries du pétrole et du gaz, y compris les énergies à faible teneur en
carbone du Comité européen de normalisation (CEN), conformément à l'Accord de coopération technique
entre l'ISO et le CEN (Accord de Vienne).
Cette troisième édition annule et remplace la deuxième édition (ISO 21809-3:2016), qui a fait l'objet d'une
révision technique. Elle incorpore également l'ISO 21809-3:2016/Amd 1:2020.
Les principales modifications sont les suivantes:
— ajout d'un programme de qualification;
— ajout de nouveaux types de FJC;
— introduction de modifications dans différents articles et paragraphes relatifs aux FJC;
— ajout de nouvelles annexes;
— introduction de modifications dans différentes annexes.
Une liste de toutes les parties de la série de normes ISO 21809 se trouve sur le site web de l'ISO.
Il convient que l'utilisateur adresse tout retour d'information ou toute question concernant le présent
document à l'organisme national de normalisation de son pays. Une liste exhaustive desdits organismes se
trouve à l'adresse www.iso.org/fr/members.html.
vii
PROJET FINAL Norme internationale ISO/FDIS 21809-3:2026(fr)
Industries du pétrole et du gaz, y compris les énergies à faible
teneur en carbone — Revêtements externes des conduites
enterrées ou immergées utilisées dans les systèmes de
transport par conduites —
Partie 3:
Revêtements des joints soudés sur site
1 Domaine d'application
Le présent document spécifie les exigences relatives aux revêtements des joints soudés sur site des tubes
en acier sans soudure et soudés destinés aux tronçons enterrés ou immergés des systèmes de transport par
conduites utilisés dans les industries du pétrole, de la pétrochimie et du gaz naturel, tels que définis dans
l'ISO 13623. Le présent document spécifie la qualification, l'application et les essais relatifs aux revêtements
de protection contre la corrosion appliqués aux surfaces d'acier laissées nues après l'assemblage des tubes et
raccords (composants) par soudage.
Le présent document définit et codifie dans le Tableau 1 les différents types de revêtement des joints soudés
sur site pour conduites.
Le présent document ne traite pas des exigences relatives à la protection mécanique supplémentaire,
l'isolation thermique ou le remplissage des joints des tubes lestés avec du béton.
NOTE Les joints soudés sur site des tubes et raccords revêtus conformément au présent document sont considérés
comme étant adaptés à une protection cathodique complémentaire.
2 Références normatives
Les documents suivants sont cités dans le texte de sorte qu'ils constituent, pour tout ou partie de leur
contenu, des exigences du présent document. Pour les références datées, seule l'édition citée s'applique. Pour
les références non datées, la dernière édition du document de référence s'applique (y compris les éventuels
amendements).
ISO 34-1, Caoutchouc vulcanisé ou thermoplastique — Détermination de la résistance au déchirement — Partie
1: Éprouvettes pantalon, angulaire et croissant
ISO 37, Caoutchouc vulcanisé ou thermoplastique — Détermination des caractéristiques de contrainte-
déformation en traction
ISO 48-4, Caoutchouc vulcanisé ou thermoplastique — Détermination de la dureté — Partie 4: Dureté par
pénétration par la méthode au duromètre (dureté Shore)
ISO 188, Caoutchouc vulcanisé ou thermoplastique — Essais de résistance au vieillissement accéléré et à la
chaleur
ISO 527-1, Plastiques — Détermination des propriétés en traction — Partie 1: Principes généraux
ISO 527-2, Plastiques — Détermination des propriétés en traction — Partie 2: Conditions d'essai des plastiques
pour moulage et extrusion
ISO 527-3, Plastiques — Détermination des propriétés en traction — Partie 3: Conditions d'essai pour films et
feuilles
ISO/FDIS 21809-3:2026(fr)
ISO 868, Plastiques et ébonite — Détermination de la dureté par pénétration au moyen d'un duromètre (dureté
Shore)
ISO 1431-1, Caoutchouc vulcanisé ou thermoplastique — Résistance au craquelage par l'ozone — Partie 1: Essais
sous allongement statique et dynamique
ISO 1817, Caoutchouc vulcanisé ou thermoplastique — Détermination de l'action des liquides
ISO 2178, Revêtement métalliques non magnétiques sur métal de base magnétique — Mesurage de l'épaisseur
du revêtement — Méthode magnétique
ISO 2808, Peintures et vernis — Détermination de l'épaisseur du feuil
ISO 3303-1, Supports textiles revêtus de caoutchouc ou de plastique — Détermination de la résistance à
l'éclatement — Partie 1: Méthode utilisant une bille d'acier
ISO 4624, Peintures et vernis — Essai de traction
ISO 6502-2, Caoutchouc — Mesure des caractéristiques de vulcanisation à l'aide de rhéomètres — Partie 2:
Rhéomètre à disque oscillant
ISO 5893, Appareils d'essai du caoutchouc et des plastiques — Types pour traction, flexion et compression
(vitesse de translation constante) — Spécifications
ISO 8501-1, Préparation des subjectiles d’acier avant application de peintures et de produits assimilés —
Évaluation visuelle de la propreté d’un subjectile — Partie 1: Degrés de rouille et degrés de préparation des
subjectiles d’acier non recouverts et des subjectiles d’acier après décapage sur toute la surface des revêtements
précédents
ISO 8501-3, Préparation des subjectiles d'acier avant application de peintures et de produits assimilés —
Évaluation visuelle de la
...