

FprEN 10160
(Main)Non-destructive testing - Ultrasonic testing of steel flat product of thickness equal to or greater than 5 mm (reflection method)
- Abstract
This document specifies a method for the ultrasonic testing of uncoated flat steel product for internal discontinuities.
This document is applicable to flat product in nominal thickness range of 5 mm to 200 mm of non-alloyed or alloyed steel, excluding austenitic or austenoferritic steels. However, this document can be applied to the latter types of steels provided that the difference between the amplitude of the noise signal and that of the echo detection threshold gives a sufficient signal to noise ratio. .
This document also defines five quality classes for the flat product body (classes S0, S1, SA, S2 and S3) and five classes (E0, E1, E2, E3, E4) for the edges (see Clause 13).
A list of equivalent terms in several European languages is given in Annex A, Table A.1.
- Status
- Not Published
- Publication Date
- 10-Feb-2027
- Technical Committee
- ECISS/TC 101 - Test methods for steel (other than chemical analysis)
- Drafting Committee
- WG 2 - Ultrasonic testing of steel flat products
FprEN 10160 is a CEN draft European Standard for ultrasonic testing of steel flat product by the reflection method. It specifies how to look for internal discontinuities in uncoated flat steel product and how to classify the product body and edges by quality class. The document is intended for producers, suppliers, purchasers, and NDT personnel who need a common acceptance and reporting method.
What does FprEN 10160 specify?
FprEN 10160 specifies a method for ultrasonic testing of uncoated flat steel product for internal discontinuities. It applies to nominal thicknesses from 5 mm to 200 mm for non-alloyed or alloyed steel, with a stated exclusion for austenitic and austenoferritic steels unless the signal-to-noise condition is suitable.
The standard organizes the subject from scope and references through terms, agreement items, principle, procedure, personnel, equipment, coupling, checking, surface condition, scanning plan, detailed test procedure, acceptance criteria, and test report. Annex A is informative and gives equivalent terms in several European languages.
| Annex | What it covers |
|---|---|
| Annex A | Equivalent terms in several European languages |
FprEN 10160 also defines five quality classes for the flat product body - S0, S1, SA, S2 and S3 - and five classes for the edges - E0 to E4. In practice, that means the order can specify different quality expectations for the body and the edges of the same product.
What are the key requirements of FprEN 10160?
FprEN 10160 requires the parties to agree key inspection details at enquiry and order stage. Clause 4 covers the manufacturing stage for testing, the volume to be examined, whether grid scanning or full coverage is needed, the quality class or classes, special equipment or couplant, the evaluation technique, the sensitivity-setting technique, purchaser presence, and whether a written procedure needs approval. That matters because the test outcome depends on what area is actually inspected and which acceptance level applies.
How the method works
Clause 5 says the method is based on reflection of ultrasonic waves with the beam axis perpendicular to the product surface. Discontinuities are located by comparing their echo amplitude with that of a flat-bottomed hole at the same depth, using DAC, DGS, or an equivalent method. For sizing, the document uses the 6 dB drop method where applicable, so the operator measures the extent of the indication rather than just noting that it exists.
Procedure, personnel, and equipment
Clause 6 requires a written procedure, which may be a product specification, a specific procedure for the application, or this document supplemented with application details. The procedure must cover the item, references, personnel qualification, manufacturing stage, examination zones, surface preparation, couplant, equipment, setting, scanning plan, operation sequence, recording levels, characterization, acceptance criteria, and report content. Clause 7 requires qualified and certified personnel under the responsibility of a qualified and certified Level 3 person in accordance with EN ISO 9712.
Clause 8 sets equipment expectations. Manual testing uses A-scan presentation and instruments that comply with the referenced equipment standards. Probes may be single-transducer, dual-transducer, or multi-transducer, but their beam axis must be perpendicular to the surface. Probe selection depends on thickness, and the document also limits dead zone, frequency range, and transducer size. Reference blocks or plates must have acoustic properties and surface condition similar to the product and cover the depth range under test.
Coupling, surface condition, and checking
Clause 9 requires a coupling medium that gives adequate contact, with the same medium used for calibration, adjustment, examination, and evaluation. Clause 10 requires routine checking of the complete manual test equipment. Clause 11 requires the scanning surface to be free from coatings, loose scale, dry couplant, irregularities, or anything that would interfere with coupling or interpretation. In practice, this means the surface preparation must be good enough to achieve the specified quality class.
Scanning and setting
Clause 12 defines the scanning plan. For the body, the document allows partial or full coverage by agreement. For classes S0, S1 and SA, scanning uses a 200 mm grid or equivalent distributed lines; for S2 and S3, it uses a 100 mm grid or equivalent distributed lines. The edges are examined over the full edge zone on all four sides, with the zone width depending on thickness.
Clause 13 sets sensitivity and range setting, scanning speed, and discontinuity sizing. For manual testing, the scanning speed must not exceed 500 mm/s. Sensitivity is based on curves from reference blocks or plates, including curves for back-wall echo and flat-bottomed holes of 11 mm, 8 mm, and 5 mm diameter depending on the quality class, with dual-transducer probes using the 5 mm hole. Only discontinuities whose echo amplitude exceeds the relevant characteristic curve are taken into account.
Acceptance and reporting
Clause 14 links the measured indications to acceptance criteria for the body and edges. The document uses separate tables for dual-transducer and single-transducer testing of the body, and separate tables for edge acceptance. Clause 15 then requires the test report to identify the supplier, order, product reference data, probe and equipment characteristics, operating conditions, results, agreed special points, date, and operator name or qualification. That gives the buyer traceability from the test settings to the reported result.
What terms does FprEN 10160 define?
FprEN 10160 defines a small set of terms that control how results are described.
- Internal discontinuity - any imperfection within the thickness of the flat product, including planar or laminar imperfections and inclusion bands or clusters.
- Defect - an internal discontinuity that exceeds the allowed size or population density limits and is therefore unacceptable.
- Population density - the number of discontinuities of a specified size range per specified area of body or length of edge zone.
- Manual and assisted manual testing - testing where an operator moves the probe and interprets ultrasonic indications directly or with signal alarm support.
- Automated and semi-automated testing - testing with mechanized probe movement and software-based data acquisition, with the operator either validating results or running the system.
- Flat-bottomed hole (FBH) - the reference reflector used to set sensitivity and compare echo amplitudes.
- Dead zone - the part of the probe response area that is effectively unusable close to the surface.
Who uses FprEN 10160?
FprEN 10160 is used by steel manufacturers, suppliers, purchasers, and NDT providers who need to inspect flat steel product for internal discontinuities. It is especially relevant where product acceptance depends on ultrasonic inspection before delivery or during production.
In practice, the standard is used by:
- production plants and suppliers carrying out routine ultrasonic inspection
- NDT operators and supervisors setting up manual, assisted manual, automated, or semi-automated tests
- quality managers defining quality classes, acceptance criteria, and report content
- purchasers who want inspection at the place of production or on the supplier's premises
- engineers and buyers who need to specify body and edge quality classes in an order
What changed in FprEN 10160 from the previous edition?
FprEN 10160 will supersede EN 10160:1999. The foreword states that the scope was modified, normative references were updated, definition 3.5 was redrafted with an added note, Clause 4 was added, Clauses 6 and 13 were expanded with more detail and guidance, a new quality class S was added in the acceptance criteria tables, Table 5 was added for dual-transducer probes, and Table 6 was added for single-transducer probes.
Which standards are used with FprEN 10160?
FprEN 10160 relies on several normative references for terminology, personnel qualification, general ultrasonic practice, and equipment verification.
- EN 1330-1 and EN 1330-2 - provide general NDT terminology used alongside the document's own definitions.
- EN ISO 5577 - gives ultrasonic testing vocabulary.
- EN ISO 9712 - defines qualification and certification for NDT personnel.
- EN ISO 16810 - gives general ultrasonic testing principles.
- EN ISO 16811 - covers sensitivity and range setting.
- EN ISO 16827 - covers characterization and sizing of discontinuities.
- EN ISO 18563-1, -2, -3 - cover characterization and verification of phased array equipment, if that equipment is used.
- EN ISO 22232-1, -2, -3 - cover characterization and verification of ultrasonic test equipment, probes, and combined equipment.
What does the FprEN 10160 document contain?
FprEN 10160 contains the working parts needed to carry out and document an ultrasonic inspection of steel flat product. It includes a scanning plan for the body and edges, settings for sensitivity and range, and acceptance criteria tied to quality classes.
The document also includes:
- probe selection guidance linked to product thickness
- reference block and flat-bottomed hole requirements
- calibration and routine checking provisions
- edge-zone dimensions by thickness
- body and edge acceptance tables for multiple quality classes
- a schematic figure for the dimensions and terms used in edge evaluation
- a test report checklist for recording the inspection result
For implementation, the document is used for production inspection, supplier inspection, order-defined acceptance, and reporting of ultrasonic findings in a form that can be checked against the agreed quality class.
Relations
- Effective Date
- 05-Oct-2024
Get Certified
Connect with accredited certification bodies for this standard
Element Materials Technology
Materials testing and product certification.

Inštitut za kovinske materiale in tehnologije
Institute of Metals and Technology. Materials testing, metallurgical analysis, NDT.
Sponsored listings
Frequently Asked Questions
FprEN 10160 is a draft published by the European Committee for Standardization (CEN). Its full title is "Non-destructive testing - Ultrasonic testing of steel flat product of thickness equal to or greater than 5 mm (reflection method)". This standard covers: This document specifies a method for the ultrasonic testing of uncoated flat steel product for internal discontinuities. This document is applicable to flat product in nominal thickness range of 5 mm to 200 mm of non-alloyed or alloyed steel, excluding austenitic or austenoferritic steels. However, this document can be applied to the latter types of steels provided that the difference between the amplitude of the noise signal and that of the echo detection threshold gives a sufficient signal to noise ratio. . This document also defines five quality classes for the flat product body (classes S0, S1, SA, S2 and S3) and five classes (E0, E1, E2, E3, E4) for the edges (see Clause 13). A list of equivalent terms in several European languages is given in Annex A, Table A.1.
This document specifies a method for the ultrasonic testing of uncoated flat steel product for internal discontinuities. This document is applicable to flat product in nominal thickness range of 5 mm to 200 mm of non-alloyed or alloyed steel, excluding austenitic or austenoferritic steels. However, this document can be applied to the latter types of steels provided that the difference between the amplitude of the noise signal and that of the echo detection threshold gives a sufficient signal to noise ratio. . This document also defines five quality classes for the flat product body (classes S0, S1, SA, S2 and S3) and five classes (E0, E1, E2, E3, E4) for the edges (see Clause 13). A list of equivalent terms in several European languages is given in Annex A, Table A.1.
FprEN 10160 is classified under the following ICS (International Classification for Standards) categories: 77.040.20 - Non-destructive testing of metals; 77.140.50 - Flat steel products and semi-products. The ICS classification helps identify the subject area and facilitates finding related standards.
FprEN 10160 has the following relationships with other standards: It is inter standard links to EN 10160:1999. Understanding these relationships helps ensure you are using the most current and applicable version of the standard.
FprEN 10160 is available in PDF format for immediate download after purchase. The document can be added to your cart and obtained through the secure checkout process. Digital delivery ensures instant access to the complete standard document.
Standards Content (Sample)
SLOVENSKI STANDARD
01-februar-2026
Neporušitvene preiskave - Ultrazvočno preskušanje ploščatih jeklenih izdelkov,
debelih 5 mm in več (tehnika impulz-odmev)
Non-destructive testing - Ultrasonic testing of steel flat product of thickness equal or
greater than 5 mm (reflection method)
Ultraschallprüfung von Flacherzeugnissen aus Stahl mit einer Dicke größer oder gleich 6
mm (Reflexionsverfahren)
Contrôle ultrasonore des produits plats en acier d'épaisseur égale ou supérieure à 6 mm
(méthode par réflexion)
Ta slovenski standard je istoveten z: prEN 10160
ICS:
77.040.20 Neporušitveno preskušanje Non-destructive testing of
kovin metals
77.140.50 Ploščati jekleni izdelki in Flat steel products and semi-
polizdelki products
2003-01.Slovenski inštitut za standardizacijo. Razmnoževanje celote ali delov tega standarda ni dovoljeno.
DRAFT
EUROPEAN STANDARD
prEN 10160
NORME EUROPÉENNE
EUROPÄISCHE NORM
January 2026
ICS 77.040.20 Will supersede EN 10160:1999
English Version
Non-destructive testing - Ultrasonic testing of steel flat
product of thickness equal or greater than 5 mm
(reflection method)
Essais non destructifs - Contrôle ultrasonore des Zerstörungsfreie Prüfung - Ultraschallprüfung von
produits plats en acier d'épaisseur égale ou supérieure Flacherzeugnissen aus Stahl mit einer Dicke größer
à 5 mm (méthode par réflexion) oder gleich 5 mm (Reflexionsverfahren)
This draft European Standard is submitted to CEN members for enquiry. It has been drawn up by the Technical Committee
CEN/TC 459/SC 1.
If this draft becomes a European Standard, CEN members are bound to comply with the CEN/CENELEC Internal Regulations
which stipulate the conditions for giving this European Standard the status of a national standard without any alteration.
This draft European Standard was established by CEN in three official versions (English, French, German). A version in any other
language made by translation under the responsibility of a CEN member into its own language and notified to the CEN-CENELEC
Management Centre has the same status as the official versions.
CEN members are the national standards bodies of Austria, Belgium, Bulgaria, Croatia, Cyprus, Czech Republic, Denmark, Estonia,
Finland, France, Germany, Greece, Hungary, Iceland, Ireland, Italy, Latvia, Lithuania, Luxembourg, Malta, Netherlands, Norway,
Poland, Portugal, Republic of North Macedonia, Romania, Serbia, Slovakia, Slovenia, Spain, Sweden, Switzerland, Türkiye and
United Kingdom.
Recipients of this draft are invited to submit, with their comments, notification of any relevant patent rights of which they are
aware and to provide supporting documentation.
Warning : This document is not a European Standard. It is distributed for review and comments. It is subject to change without
notice and shall not be referred to as a European Standard.
EUROPEAN COMMITTEE FOR STANDARDIZATION
COMITÉ EUROPÉEN DE NORMALISATION
EUROPÄISCHES KOMITEE FÜR NORMUNG
CEN-CENELEC Management Centre: Rue de la Science 23, B-1040 Brussels
© 2026 CEN All rights of exploitation in any form and by any means reserved Ref. No. prEN 10160:2026 E
worldwide for CEN national Members.
prEN 10160:2025(E)
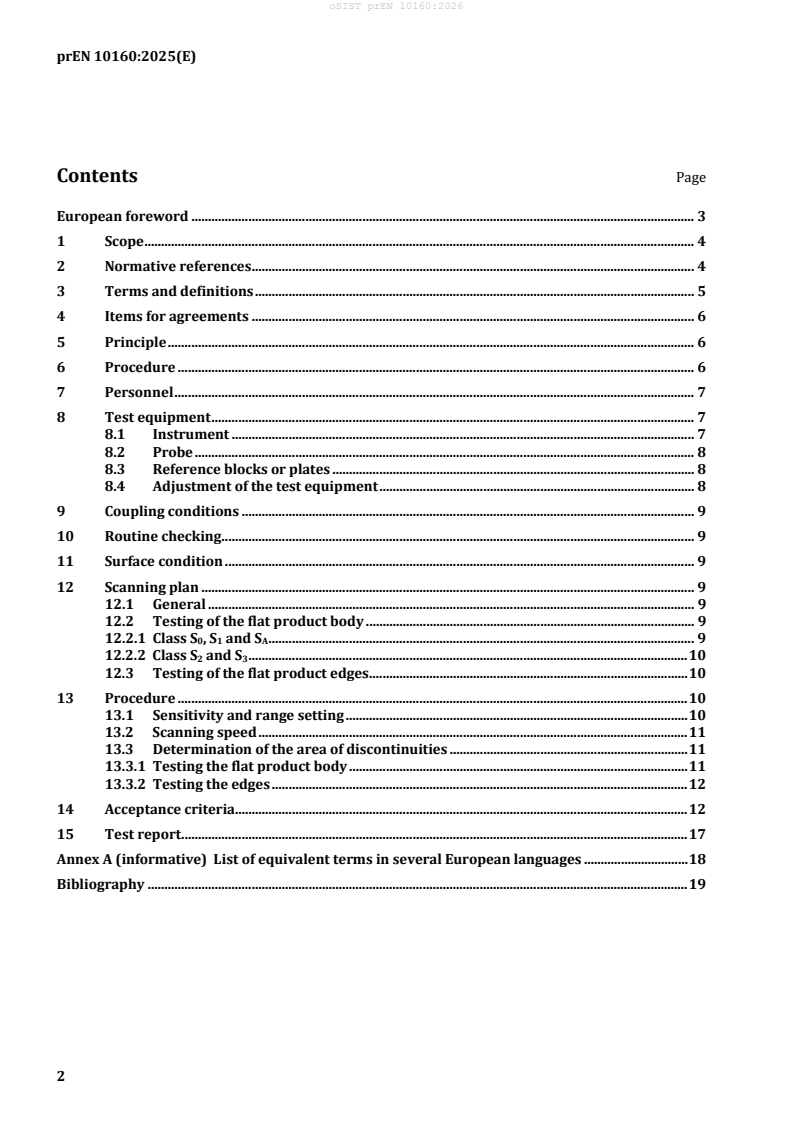
Contents Page
European foreword . 3
1 Scope . 4
2 Normative references . 4
3 Terms and definitions . 5
4 Items for agreements . 6
5 Principle . 6
6 Procedure . 6
7 Personnel . 7
8 Test equipment . 7
8.1 Instrument . 7
8.2 Probe . 8
8.3 Reference blocks or plates . 8
8.4 Adjustment of the test equipment . 8
9 Coupling conditions . 9
10 Routine checking . 9
11 Surface condition . 9
12 Scanning plan . 9
12.1 General . 9
12.2 Testing of the flat product body . 9
12.2.1 Class S , S and S . 9
0 1 A
12.2.2 Class S and S . 10
2 3
12.3 Testing of the flat product edges . 10
13 Procedure . 10
13.1 Sensitivity and range setting . 10
13.2 Scanning speed . 11
13.3 Determination of the area of discontinuities . 11
13.3.1 Testing the flat product body . 11
13.3.2 Testing the edges . 12
14 Acceptance criteria. 12
15 Test report . 17
Annex A (informative) List of equivalent terms in several European languages . 18
Bibliography . 19
prEN 10160:2025(E)
European foreword
This document (prEN 10160:2025) has been prepared by Technical Committee CEN/TC 459/SC 1 “Test
methods for steel (other than chemical analysis)”, the secretariat of which is held by AFNOR.
This document is currently submitted to the CEN Enquiry.
This document will supersede EN 10160:1999.
prEN 10160:2025 includes the following significant technical changes with respect to EN 10160:1999:
— The Scope was modified: thickness extended and new quality class added;
— Normative references updated;
— Definition 3.5 redrafted and a Note 1 to entry added;
— Clause 4 Items for agreement: added;
— Clause 6 – Procedure and Clause 13 – Operation procedure: more details and guidelines added;
— A new quality class S as an acceptance criteria in Tables 3 and 4 was added;
A
— Table 5 was added only for dual-transducer probes;
— Table 6 was added to give acceptance criteria for single-tranducer probes.
prEN 10160:2025(E)
1 Scope
This document describes a method for the ultrasonic testing of uncoated flat steel product for internal
discontinuities.
This document is applicable to flat product in nominal thickness range of 5 mm to 200 mm of non-
alloyed or alloyed steel, excluding austenitic or austenoferritic steels. However, this document can be
applied to the latter types of steels provided that the difference between the amplitude of the noise
signal and that of the echo detection threshold is sufficient for the limit fixed.
This document also defines five quality classes for the flat product body (classes S , S , S , S and S ) and
0 1 A 2 3
five classes (E , E , E , E , E ) for the edges (see Clause 13).
0 1 2 3 4
Other methods of testing (e.g. by phased-array) or other test equipment may be used at the
manufacturer's discretion provided that they give identical results to those obtained under the
conditions of this document. In the event of a dispute, only the method defined in this document shall
prevail.
Testing of flat product of thickness less than 5 mm or higher than 200 mm may be the subject of special
agreements between the parties concerned.
The inspection is normally carried out in the place of production or on the premises of the supplier. If
specified on the order, the inspection takes place in the presence of the purchaser or his
representative .
A list of equivalent terms in several European languages is given in Annex A.
2 Normative references
The following documents are referred to in the text in such a way that some or all of their content
constitutes requirements of this document. For dated references, only the edition cited applies. For
undated references, the latest edition of the referenced document (including any amendments) applies.
EN 1330-1, Non-destructive testing — Terminology – Part 1: List of general terms
EN 1330-2, Non-destructive testing— Terminology — Part 2: Terms common to the non-destructive
testing methods
EN ISO 5577, Non-destructive testing — Ultrasonic testing — Vocabulary (ISO 5577)
EN ISO 9712, Non-destructive testing — Qualification and certification of NDT personnel (ISO 9712)
EN ISO 16810, Non-destructive testing — Ultrasonic testing — General principles (ISO 16810)
EN ISO 16811, Non-destructive testing — Ultrasonic testing — Sensitivity and range setting (ISO 16811)
EN ISO 16827, Non-destructive testing — Ultrasonic testing — Characterization and sizing of
discontinuities (ISO 16827)
EN ISO 18563-1, Non-destructive testing — Characterization and verification of ultrasonic phased array
equipment — Part 1: Instruments (ISO 18563-1)
EN ISO 18563-2, Non-destructive testing — Characterization and verification of ultrasonic phased array
equipment — Part 2: Array probes (ISO 18563-2)
In this case, all steps should be taken to ensure that the production process is not disturbed.
prEN 10160:2025(E)
EN ISO 18563-3, Non-destructive testing — Characterization and verification of ultrasonic phased array
equipment — Part 3: Complete systems (ISO 18563-3)
EN ISO 22232-1, Non-destructive testing — Characterization and verification of ultrasonic test
equipment — Part 1: Instruments (ISO 22232-1)
EN ISO 22232-2, Non-destructive testing — Characterization and verification of ultrasonic test
equipment — Part 2: Probes (ISO 22232-2)
EN ISO 22232-3, Non-destructive testing — Characterization and verification of ultrasonic test
equipment — Part 3: Combined equipment (ISO 22232-3)
3 Terms and definitions
For the purposes of this document, the terms and definitions given in EN 1330-1, EN 1330-2,
EN ISO 5577 and the following apply.
ISO and IEC maintain terminology databases for use in standardization at the following addresses:
— ISO Online browsing platform: available at https://www.iso.org/obp/
— IEC Electropedia: available at https://www.electropedia.org/
3.1
internal discontinuity
any imperfection lying within the thickness of the flat product, e.g planar or laminar imperfection,
single-plane or multi-plane inclusion bands or clusters
Note 1 to entry: It is referred to in the text as discontinuity.
3.2
defect
unacceptable internal discontinuity, i.e. exceeding the specified maximum size or population density
limits
3.3
population density
number of individual internal discontinuities of a size greater than a specified minimum size and less
than a specified maximum size per specified area of body or length of edge zone
3.4
manual and assisted manual testing
testing by an operator applying an ultrasonic probe, or probes, to the flat product surface, manually
executing the appropriate scanning pattern on the flat product surface and visually assessing ultrasonic
signal indications on the ultrasonic instrument either by direct viewing or by built-in signal amplitude
alarm devices
3.5
automated and semi-automated testing
testing using a mechanized means of applying the ultrasonic probe or probes to, and executing the
appropriate scanning pattern on the flat product surface, together with ultrasonic signal indication
evaluation by using fully automated software-based data acquisition
Note 1 to entry: Such testing shall be either fully automatic or semi-automatic when the operator performs basic
equipment operation functions and validates testing results.
prEN 10160:2025(E)
4 Items for agreements
The following aspects of ultrasonic testing may be agreed at the time of enquiry and order:
a) the manufacturing stage(s) at which ultrasonic testing shall be performed (see Clause 10);
b) the volume(s) to be tested and whether grid scanning coverage or complete scanning coverage is
required (see Clause 13);
c) the Quality Class required, or the Quality Classes and the zones to which they apply (see Clause 15);
d) the applicable recording level and acceptance criteria if different from those detailed in Table 3,
Table 4, Table 5 and Table 6;
e) whether any special scanning coverage, equipment or couplant is required in addition to that
detailed in Clauses 8 and 13;
f) the techniques to evaluate discontinuities (see Clause 14);
g) the technique(s) to be used for setting sensitivity (see Clause 12);
h) whether the test is to be conducted in the presence of the purchaser or his representative;
i) whether a written procedure shall be submitted for approval by the purchaser (see Clause 6).
5 Principle
The method used shall be based on the reflection of ultrasonic waves, the beam axis of which is
perpendicular to the surface of the product.
The examination shall consist of:
a) locating any discontinuity by comparing the amplitude of the discontinuity echo with the amplitude
of the echo of a flat-bottomed hole of a given diameter and located at the same depth as the
discontinuity (DAC, DGS, or equivalent methods);
NOTE Only those discontinuities giving an echo higher in amplitude to that of the echo obtained with the
reference flat-bottomed hole are taken into consideration.
b) if applicable according to Clause 14, determining the contour of the discontinuity being defined by
the positions of the centre of the probe corresponding to an echo amplitude of half the maximum
amplitude of the discontinuity under consideration (6 dB drop method). The width of the
discontinuity shall be determined perpendicular to the direction of rolling. The length shall be
determined in the rolling direction.
The examination shall be carried out during the first ultrasonic scan for all the flat product thicknesses
and from one side only.
6 Procedure
The testing shall be carried out in the place of production or on the premises of the supplier. If specified
on the order, the testing may take place in the presence of the purchaser or his representative (see
Clause 4 h)).
prEN 10160:2025(E)
Ultrasonic testing shall be performed in accordance with a written procedure. Where specified in the
enquiry or order, the written procedure shall be submitted to the purchaser for approval prior to
testing.
This written procedure shall be in the form of:
— a product specification; or
— a procedure written specifically for the application; or
— this document may be used if it is accompanied by examination details specific to the application.
The procedure shall contain the following details as a minimum requirement:
a) description of the item to be examined;
b) reference documents;
c) qualification and certification of examination personnel;
d) stage of manufacture at which the examination is carried out;
e) examination zones specified in terms of the applicable Quality Classes;
f) any special preparation of scanning surfaces, if applicable;
g) couplant;
h) description of examination equipment;
i) setting;
j) scanning plan;
k) description and sequence of examination operations;
l) recording levels;
m) characterization of discontinuities;
n) acceptance criteria;
o) examination report.
7 Personnel
Testing shall be carried out by a qualified and certified personnel under the responsibility of a qualified
and certified Level 3 personnel in accordance with EN ISO 9712.
8 Test equipment
8.1 Instrument
Instrument for manual testing shall feature A-scan presentation and shall comply with the
requirements of EN ISO 22232-1. or EN ISO 18563-1, if applicable.
prEN 10160:2025(E)
8.2 Probe
The probe used for testing shall comply with the requirements of EN ISO 22232-2 or EN ISO 18563-2.
The test equipment shall include at least one probe which may be either a probe with a single
transducer serving
...