


ASTM B545-13(2021)
(Specification)Standard Specification for Electrodeposited Coatings of Tin
Standard Specification for Electrodeposited Coatings of Tin
ABSTRACT
This specification covers the requirements for electrodeposited tin coatings applied to metallic articles to provide a low contact resistance surface, to protect against corrosion, to facilitate soldering, to provide anti-galling properties, and to be a stop-off coating in the nitriding of high-strength steels. This specification does not cover hot-dipped tin or other non-electrodeposited coatings, and mill products. Coatings shall be grouped into six service classes, which is based on the minimum thickness and severity of service required for the coating, and three surface appearance types, which is based on the type electroplating process employed. The surface appearance types are matte tin electrodeposits, bright tin electrodeposits, and flow-brightened electrodeposits. Coatings shall be sampled, tested and conform accordingly to specified requirements as to appearance, purity, local and mean thickness, integrity (including gross defects, mechanical damage, and porosity), adhesion, solderability, and hydrogen embrittlement relief.
SCOPE
1.1 This specification covers the requirements for electrodeposited (electroplated) coatings of tin applied to metallic articles. Tin coatings are used to provide a low contact-resistance surface, to protect against corrosion (see 1.2), to facilitate soldering, to provide anti-galling properties, and to be a stopoff coating in the nitriding of high-strength steels.
1.2 Some corrosion can be expected from tin coatings exposed outdoors. In normal indoor exposure, tin is protective on iron, steel, nickel, copper, and their alloys. Corrosion can be expected at discontinuities in the coating (such as pores) due to galvanic couples formed between the tin and the underlying metal through the discontinuities, especially in humid atmospheres. Porosity increases as the coating thickness decreases, so that minimum thicknesses must be specified for each application. Parts coated with tin can be assembled safely in contact with iron and steel, tin-coated aluminum, yellow chromated zinc, cadmium, and solder coatings. (See X5.1 for oxidation and corrosion properties.)
1.3 This specification applies to electroplated coatings of not less than 99 % tin (except where deliberately alloyed for special purposes, as stated in X6.3) obtained from any of the available tin electroplating processes (see 4.3).
1.4 This specification does not apply to hot-dipped tin or other non-electrodeposited coating; it also does not apply to mill products. For mill products, refer to Specifications A623 or A623M.
1.5 The values stated in SI units are to be regarded as the standard. The values given in parentheses are for information only.
1.6 This standard does not purport to address all of the safety concerns, if any, associated with its use. It is the responsibility of the user of this standard to establish appropriate safety, health, and environmental practices and determine the applicability of regulatory limitations prior to use.
1.7 This international standard was developed in accordance with internationally recognized principles on standardization established in the Decision on Principles for the Development of International Standards, Guides and Recommendations issued by the World Trade Organization Technical Barriers to Trade (TBT) Committee.
General Information
Buy Standard


Standards Content (Sample)
NOTICE: This standard has either been superseded and replaced by a new version or withdrawn.
Contact ASTM International (www.astm.org) for the latest information
Designation:B545 −13 (Reapproved 2021)
Standard Specification for
Electrodeposited Coatings of Tin
This standard is issued under the fixed designation B545; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision.Anumber in parentheses indicates the year of last reapproval.A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
This standard has been approved for use by agencies of the U.S. Department of Defense.
1. Scope 1.7 This international standard was developed in accor-
dance with internationally recognized principles on standard-
1.1 Thisspecificationcoverstherequirementsforelectrode-
ization established in the Decision on Principles for the
posited (electroplated) coatings of tin applied to metallic
Development of International Standards, Guides and Recom-
articles. Tin coatings are used to provide a low contact-
mendations issued by the World Trade Organization Technical
resistance surface, to protect against corrosion (see 1.2), to
Barriers to Trade (TBT) Committee.
facilitatesoldering,toprovideanti-gallingproperties,andtobe
a stopoff coating in the nitriding of high-strength steels.
2. Referenced Documents
1.2 Some corrosion can be expected from tin coatings
2.1 ASTM Standards:
exposed outdoors. In normal indoor exposure, tin is protective
A623Specification for Tin Mill Products, General Require-
oniron,steel,nickel,copper,andtheiralloys.Corrosioncanbe
ments
expectedatdiscontinuitiesinthecoating(suchaspores)dueto
A623MSpecification for Tin Mill Products, General Re-
galvanic couples formed between the tin and the underlying
quirements [Metric]
metal through the discontinuities, especially in humid atmo-
B32Specification for Solder Metal
spheres. Porosity increases as the coating thickness decreases,
B183Practice for Preparation of Low-Carbon Steel for
so that minimum thicknesses must be specified for each
Electroplating
application. Parts coated with tin can be assembled safely in
B242Guide for Preparation of High-Carbon Steel for Elec-
contact with iron and steel, tin-coated aluminum, yellow
troplating
chromated zinc, cadmium, and solder coatings. (See X5.1 for
B246Specification for Tinned Hard-Drawn and Medium-
oxidation and corrosion properties.)
Hard-Drawn Copper Wire for Electrical Purposes
1.3 This specification applies to electroplated coatings of
B281Practice for Preparation of Copper and Copper-Base
not less than 99% tin (except where deliberately alloyed for
Alloys for Electroplating and Conversion Coatings
special purposes, as stated in X6.3) obtained from any of the
B320Practice for Preparation of Iron Castings for Electro-
available tin electroplating processes (see 4.3).
plating
B322Guide for Cleaning Metals Prior to Electroplating
1.4 This specification does not apply to hot-dipped tin or
B374Terminology Relating to Electroplating
other non-electrodeposited coating; it also does not apply to
B487Test Method for Measurement of Metal and Oxide
mill products. For mill products, refer to Specifications A623
Coating Thickness by Microscopical Examination of
or A623M.
Cross Section
1.5 The values stated in SI units are to be regarded as the
B499Test Method for Measurement of CoatingThicknesses
standard. The values given in parentheses are for information
by the Magnetic Method: Nonmagnetic Coatings on
only.
Magnetic Basis Metals
1.6 This standard does not purport to address all of the
B504Test Method for Measurement of Thickness of Metal-
safety concerns, if any, associated with its use. It is the
lic Coatings by the Coulometric Method
responsibility of the user of this standard to establish appro-
B507Practice for Design ofArticles to Be Electroplated on
priate safety, health, and environmental practices and deter-
Racks
mine the applicability of regulatory limitations prior to use.
B542Terminology Relating to Electrical Contacts andTheir
Use
This specification is under the jurisdiction of ASTM Committee B08 on
Metallic and Inorganic Coatings and is the direct responsibility of Subcommittee
B08.06 on Soft Metals. For referenced ASTM standards, visit the ASTM website, www.astm.org, or
Current edition approved May 1, 2021. Published May 2021. Originally contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM
approved in 1971. Last previous edition approved in 2013 as B545–13. DOI: Standards volume information, refer to the standard’s Document Summary page on
10.1520/B0545-13R21. the ASTM website.
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
B545−13 (2021)
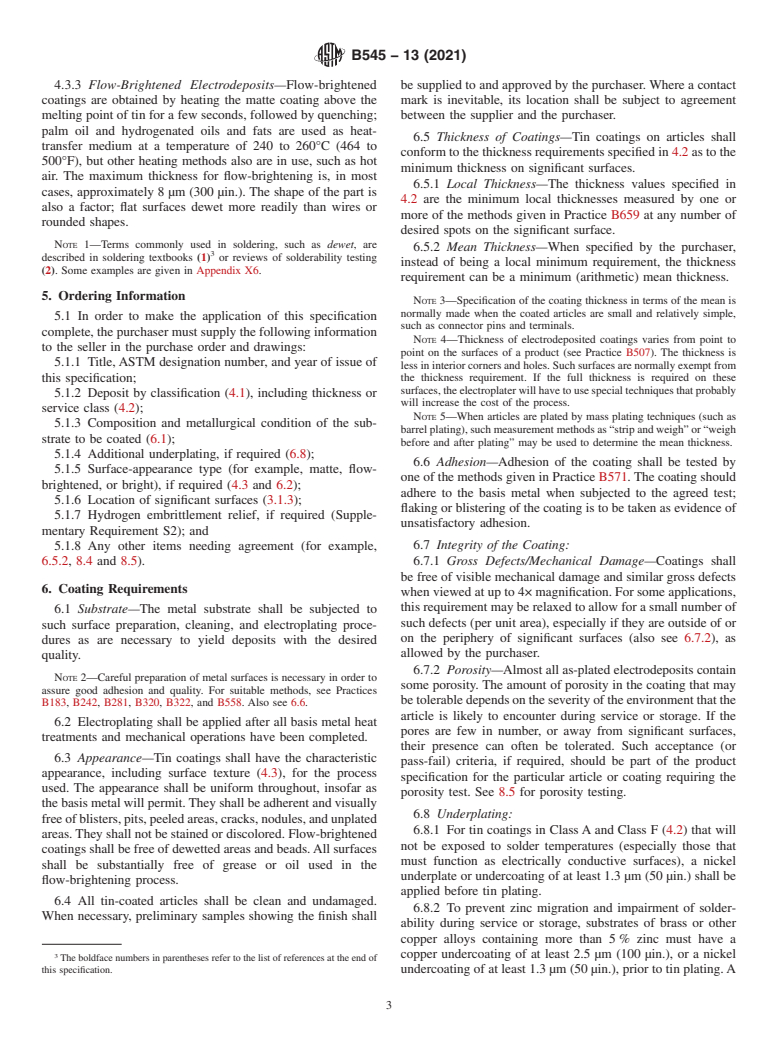
B558Practice for Preparation of Nickel Alloys for Electro- 4. Classification
plating
4.1 General—Orders for articles to be plated in accordance
B567Test Method for Measurement of Coating Thickness
with this specification shall specify the service class (4.2) (and
by the Beta Backscatter Method
underplating, if required), indicating the severity of service
B568Test Method for Measurement of Coating Thickness
required for the coating. Other coatings variations, such as
by X-Ray Spectrometry
surface appearance type (4.3) or alloy composition (Appendix
B571Practice for Qualitative Adhesion Testing of Metallic
X6), are optional.
Coatings
B602Test Method for Attribute Sampling of Metallic and
4.2 Service Class:
Inorganic Coatings
Class Minimum Thickness Typical Applications
B659Guide for Measuring Thickness of Metallic and Inor-
A 2.5 µm (100 µin.) Mild service conditions, particularly where the
ganic Coatings
significant surface is shielded from the
B678Test Method for Solderability of Metallic-Coated atmosphere (as in electronic connector
housings). To provide corrosion and tarnish
Products
resistance where greater thicknesses may be
B697Guide for Selection of Sampling Plans for Inspection
detrimental to the mechanical operation of the
product (for example, small electrical spring
of Electrodeposited Metallic and Inorganic Coatings
contacts and relays). Class A is often used for
B762Test Method of Variables Sampling of Metallic and
tin coatings that are not to be soldered, but
Inorganic Coatings
must function as low-resistance electrical
contact surfaces.
B765GuideforSelectionofPorosityandGrossDefectTests
B 5 µm (200 µin.) Mild service conditions with less severe
for Electrodeposits and Related Metallic Coatings
requirements than Class C (below).
Applications are as follows: precoating on
B809Test Method for Porosity in Metallic Coatings by
solderable basis metals to facilitate the
Humid Sulfur Vapor (“Flowers-of-Sulfur”)
soldering of electrical components; as a surface
B849Specification for Pre-Treatments of Iron or Steel for preparation for protective painting; for
antigalling purposes; and as a stopoff in
Reducing Risk of Hydrogen Embrittlement
nitriding. Also found on baking pans after
B850GuideforPost-CoatingTreatmentsofSteelforReduc-
reflow.
C 8 µm (320 µin.), Moderate exposure conditions, usually indoors,
ing the Risk of Hydrogen Embrittlement
(10 µm (400 µin.) but more severe than Class B. Examples are
B851Specification for Automated Controlled Shot Peening
for steel substrates) electrical hardware (such as cases for relays
of MetallicArticles Prior to Nickel,Autocatalytic Nickel,
and coils, transformer cans, screened cages,
chassis, frames, and fittings) and for retention
or Chromium Plating, or as Final Finish
of the solderability of solderable articles during
D3951Practice for Commercial Packaging
storage.
D 15 µm (600 µin.) Severe service, including exposure to
(20 µm (800 µin.) dampness and mild corrosion from moderate
3. Terminology
for steel substrates) industrial environments. Examples are fittings
for gas meters, automotive accessories (such
3.1 Definitions:
as air cleaners and oil filters), and in some
3.1.1 Many of the terms used in this specification are electronic applications.
E 30 µm (0.0012 in.) Very severe service conditions, including
defined in Terminology B374 or B542.
elevated temperatures, where underlying metal
diffusion and intermetallic formation processes
3.1.2 rack-plating—an electrodeposition process in which
are accelerated. Thicknesses of 30 to 125 µm
articles to be coated are mounted on racks or other fixtures
(0.0012 to 0.005 in.) may be required if the
during the process.
coating is subjected to abrasion or is exposed
to slowly corrosive liquids or corrosive
3.1.3 significant surface—that portion of the surface of a
atmospheres or gases. Thicker coatings are
used for water containers, threaded steel
coatedarticleatwhichthecoatingisrequiredtomeetallofthe
couplings of oil drilling strings, and seacoast
requirements of the coating specification for that article;
atmospheres. Coatings subject to mild etchants
significant surfaces are usually those that are essential to the are included.
F 1.5 µm (60 µin.) Similar to Class A, but for shorter-term contact
serviceability or function of the article, or that can be a source
applications and short shelf-life requirements,
of corrosion products or tarnish films that interfere with the
subject to purchaser approval.
function or desirable appearance of the article; significant
4.3 Surface Appearance Type (Electroplating Process):
surfaces shall be indicated on the drawings of the parts or by
4.3.1 Matte Tin Electrodeposits—Coatings with a matte
the provision of suitably marked samples.
appearance are obtained from tin plating baths (stannate,
3.1.4 undercoating (see 3.1.5)—also called an underplate in
sulfate, methylsulfonate, and fluoborate) used without the
the electronics industry.
addition of any brightening agents. However, all matte baths
(except for stannate baths) do require the addition of grain-
3.1.5 underplating—application of a metallic coating layer
refiners, and often of other additives in order to produce the
between the basis metal or substrate and the topmost metallic
desired matte finish.
coating or coatings. The thickness of such an undercoating is
4.3.2 Bright Tin Electrodeposits—Bright coatings are ob-
usually greater than 0.8 µm (30 µin.). This is in contrast to
strikes or flashes, whose thicknesses are generally much tained when proprietary brightening agents are used in specific
smaller. bright tin plating baths.
B545−13 (2021)
4.3.3 Flow-Brightened Electrodeposits—Flow-brightened be supplied to and approved by the purchaser.Where a contact
coatings are obtained by heating the matte coating above the mark is inevitable, its location shall be subject to agreement
melting point of tin for a few seconds, followed by quenching; between the supplier and the purchaser.
palm oil and hydrogenated oils and fats are used as heat-
6.5 Thickness of Coatings—Tin coatings on articles shall
transfer medium at a temperature of 240 to 260°C (464 to
conformtothethicknessrequirementsspecifiedin4.2astothe
500°F), but other heating methods also are in use, such as hot
minimum thickness on significant surfaces.
air. The maximum thickness for flow-brightening is, in most
6.5.1 Local Thickness—The thickness values specified in
cases, approximately 8 µm (300 µin.). The shape of the part is
4.2 are the minimum local thicknesses measured by one or
also a factor; flat surfaces dewet more readily than wires or
more of the methods given in Practice B659 at any number of
rounded shapes.
desired spots on the significant surface.
NOTE 1—Terms commonly used in soldering, such as dewet, are
6.5.2 Mean Thickness—When specified by the purchaser,
described in soldering textbooks (1) or reviews of solderability testing
instead of being a local minimum requirement, the thickness
(2). Some examples are given in Appendix X6.
requirement can be a minimum (arithmetic) mean thickness.
5. Ordering Information
NOTE 3—Specification of the coating thickness in terms of the mean is
normally made when the coated articles are small and relatively simple,
5.1 In order to make the application of this specification
such as connector pins and terminals.
complete,thepurchasermustsupplythefollowinginformation
NOTE 4—Thickness of electrodeposited coatings varies from point to
to the seller in the purchase order and drawings:
point on the surfaces of a product (see Practice B507). The thickness is
5.1.1 Title,ASTM designation number, and year of issue of
lessininteriorcornersandholes.Suchsurfacesarenormallyexemptfrom
this specification; the thickness requirement. If the full thickness is required on these
surfaces,theelectroplaterwillhavetousespecialtechniquesthatprobably
5.1.2 Deposit by classification (4.1), including thickness or
will increase the cost of the process.
service class (4.2);
NOTE 5—When articles are plated by mass plating techniques (such as
5.1.3 Composition and metallurgical condition of the sub-
barrelplating),suchmeasurementmethodsas“stripandweigh”or“weigh
strate to be coated (6.1);
before and after plating” may be used to determine the mean thickness.
5.1.4 Additional underplating, if required (6.8);
6.6 Adhesion—Adhesion of the coating shall be tested by
5.1.5 Surface-appearance type (for example, matte, flow-
oneofthemethodsgiveninPracticeB571.Thecoatingshould
brightened, or bright), if required (4.3 and 6.2);
adhere to the basis metal when subjected to the agreed test;
5.1.6 Location of significant surfaces (3.1.3);
flakingorblisteringofthecoatingistobetakenasevidenceof
5.1.7 Hydrogen embrittlement relief, if required (Supple-
unsatisfactory adhesion.
mentary Requirement S2); and
5.1.8 Any other items needing agreement (for example, 6.7 Integrity of the Coating:
6.5.2, 8.4 and 8.5). 6.7.1 Gross Defects/Mechanical Damage—Coatings shall
be free of visible mechanical damage and similar gross defects
6. Coating Requirements
whenviewedatupto4×magnification.Forsomeapplications,
thisrequirementmayberelaxedtoallowforasmallnumberof
6.1 Substrate—The metal substrate shall be subjected to
such defects (per unit area), especially if they are outside of or
such surface preparation, cleaning, and electroplating proce-
on the periphery of significant surfaces (also see 6.7.2), as
dures as are necessary to yield deposits with the desired
allowed by the purchaser.
quality.
6.7.2 Porosity—Almostallas-platedelectrodepositscontain
NOTE 2—Careful preparation of metal surfaces is necessary in order to
some porosity. The amount of porosity in the coating that may
assure good adhesion and quality. For suitable methods, see Practices
betolerabledependsontheseverityoftheenvironmentthatthe
B183, B242, B281, B320, B322, and B558. Also see 6.6.
article is likely to encounter during service or storage. If the
6.2 Electroplating shall be applied after all basis metal heat
pores are few in number, or away from significant surfaces,
treatments and mechanical o
...
This document is not an ASTM standard and is intended only to provide the user of an ASTM standard an indication of what changes have been made to the previous version. Because
it may not be technically possible to adequately depict all changes accurately, ASTM recommends that users consult prior editions as appropriate. In all cases only the current version
of the standard as published by ASTM is to be considered the official document.
Designation: B545 − 13 B545 − 13 (Reapproved 2021)
Standard Specification for
Electrodeposited Coatings of Tin
This standard is issued under the fixed designation B545; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision. A number in parentheses indicates the year of last reapproval. A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
This standard has been approved for use by agencies of the U.S. Department of Defense.
1. Scope
1.1 This specification covers the requirements for electrodeposited (electroplated) coatings of tin applied to metallic articles. Tin
coatings are used to provide a low contact-resistance surface, to protect against corrosion (see 1.2), to facilitate soldering, to
provide anti-galling properties, and to be a stopoff coating in the nitriding of high-strength steels.
1.2 Some corrosion can be expected from tin coatings exposed outdoors. In normal indoor exposure, tin is protective on iron, steel,
nickel, copper, and their alloys. Corrosion can be expected at discontinuities in the coating (such as pores) due to galvanic couples
formed between the tin and the underlying metal through the discontinuities, especially in humid atmospheres. Porosity increases
as the coating thickness decreases, so that minimum thicknesses must be specified for each application. Parts coated with tin can
be assembled safely in contact with iron and steel, tin-coated aluminum, yellow chromated zinc, cadmium, and solder coatings.
(See X5.1 for oxidation and corrosion properties.)
1.3 This specification applies to electroplated coatings of not less than 99 % tin (except where deliberately alloyed for special
purposes, as stated in X6.3) obtained from any of the available tin electroplating processes (see 4.3).
1.4 This specification does not apply to hot-dipped tin or other non-electrodeposited coating; it also does not apply to mill
products. For mill products, refer to Specifications A623 or A623M.
1.5 The values stated in SI units are to be regarded as the standard. The values given in parentheses are for information only.
1.6 This standard does not purport to address all of the safety concerns, if any, associated with its use. It is the responsibility
of the user of this standard to establish appropriate safety safety, health, and healthenvironmental practices and determine the
applicability of regulatory limitations prior to use.
1.7 This international standard was developed in accordance with internationally recognized principles on standardization
established in the Decision on Principles for the Development of International Standards, Guides and Recommendations issued
by the World Trade Organization Technical Barriers to Trade (TBT) Committee.
2. Referenced Documents
2.1 ASTM Standards:
A623 Specification for Tin Mill Products, General Requirements
This specification is under the jurisdiction of ASTM Committee B08 on Metallic and Inorganic Coatings and is the direct responsibility of Subcommittee B08.06 on Soft
Metals.
Current edition approved May 1, 2013May 1, 2021. Published July 2013May 2021. Originally approved in 1971. Last previous edition approved in 20092013 as B545 – 97
(2009).B545 – 13. DOI: 10.1520/B0545-13.10.1520/B0545-13R21.
For referenced ASTM standards, visit the ASTM website, www.astm.org, or contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM Standards
volume information, refer to the standard’s Document Summary page on the ASTM website.
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
B545 − 13 (2021)
A623M Specification for Tin Mill Products, General Requirements [Metric]
B32 Specification for Solder Metal
B183 Practice for Preparation of Low-Carbon Steel for Electroplating
B242 Guide for Preparation of High-Carbon Steel for Electroplating
B246 Specification for Tinned Hard-Drawn and Medium-Hard-Drawn Copper Wire for Electrical Purposes
B281 Practice for Preparation of Copper and Copper-Base Alloys for Electroplating and Conversion Coatings
B320 Practice for Preparation of Iron Castings for Electroplating
B322 Guide for Cleaning Metals Prior to Electroplating
B374 Terminology Relating to Electroplating
B487 Test Method for Measurement of Metal and Oxide Coating Thickness by Microscopical Examination of Cross Section
B499 Test Method for Measurement of Coating Thicknesses by the Magnetic Method: Nonmagnetic Coatings on Magnetic Basis
Metals
B504 Test Method for Measurement of Thickness of Metallic Coatings by the Coulometric Method
B507 Practice for Design of Articles to Be Electroplated on Racks
B542 Terminology Relating to Electrical Contacts and Their Use
B558 Practice for Preparation of Nickel Alloys for Electroplating
B567 Test Method for Measurement of Coating Thickness by the Beta Backscatter Method
B568 Test Method for Measurement of Coating Thickness by X-Ray Spectrometry
B571 Practice for Qualitative Adhesion Testing of Metallic Coatings
B602 Test Method for Attribute Sampling of Metallic and Inorganic Coatings
B659 Guide for Measuring Thickness of Metallic and Inorganic Coatings
B678 Test Method for Solderability of Metallic-Coated Products
B697 Guide for Selection of Sampling Plans for Inspection of Electrodeposited Metallic and Inorganic Coatings
B762 Test Method of Variables Sampling of Metallic and Inorganic Coatings
B765 Guide for Selection of Porosity and Gross Defect Tests for Electrodeposits and Related Metallic Coatings
B809 Test Method for Porosity in Metallic Coatings by Humid Sulfur Vapor (“Flowers-of-Sulfur”)
B849 Specification for Pre-Treatments of Iron or Steel for Reducing Risk of Hydrogen Embrittlement
B850 Guide for Post-Coating Treatments of Steel for Reducing the Risk of Hydrogen Embrittlement
B851 Specification for Automated Controlled Shot Peening of Metallic Articles Prior to Nickel, Autocatalytic Nickel, or
Chromium Plating, or as Final Finish
D3951 Practice for Commercial Packaging
3. Terminology
3.1 Definitions:
3.1.1 Many of the terms used in this specification are defined in Terminology B374 or B542.
3.1.2 rack-plating—an electrodeposition process in which articles to be coated are mounted on racks or other fixtures during the
process.
3.1.3 significant surface—that portion of the surface of a coated article at which the coating is required to meet all of the
requirements of the coating specification for that article; significant surfaces are usually those that are essential to the serviceability
or function of the article, or that can be a source of corrosion products or tarnish films that interfere with the function or desirable
appearance of the article; significant surfaces shall be indicated on the drawings of the parts or by the provision of suitably marked
samples.
3.1.4 undercoating (see 3.1.5)—also called an underplate in the electronics industry.
3.1.5 underplating—application of a metallic coating layer between the basis metal or substrate and the topmost metallic coating
or coatings. The thickness of such an undercoating is usually greater than 0.8 μm (30 μin.). This is in contrast to strikes or flashes,
whose thicknesses are generally much smaller.
4. Classification
4.1 General—Orders for articles to be plated in accordance with this specification shall specify the service class (4.2) (and
underplating, if required), indicating the severity of service required for the coating. Other coatings variations, such as surface
appearance type (4.3) or alloy composition (Appendix X6), are optional.
B545 − 13 (2021)
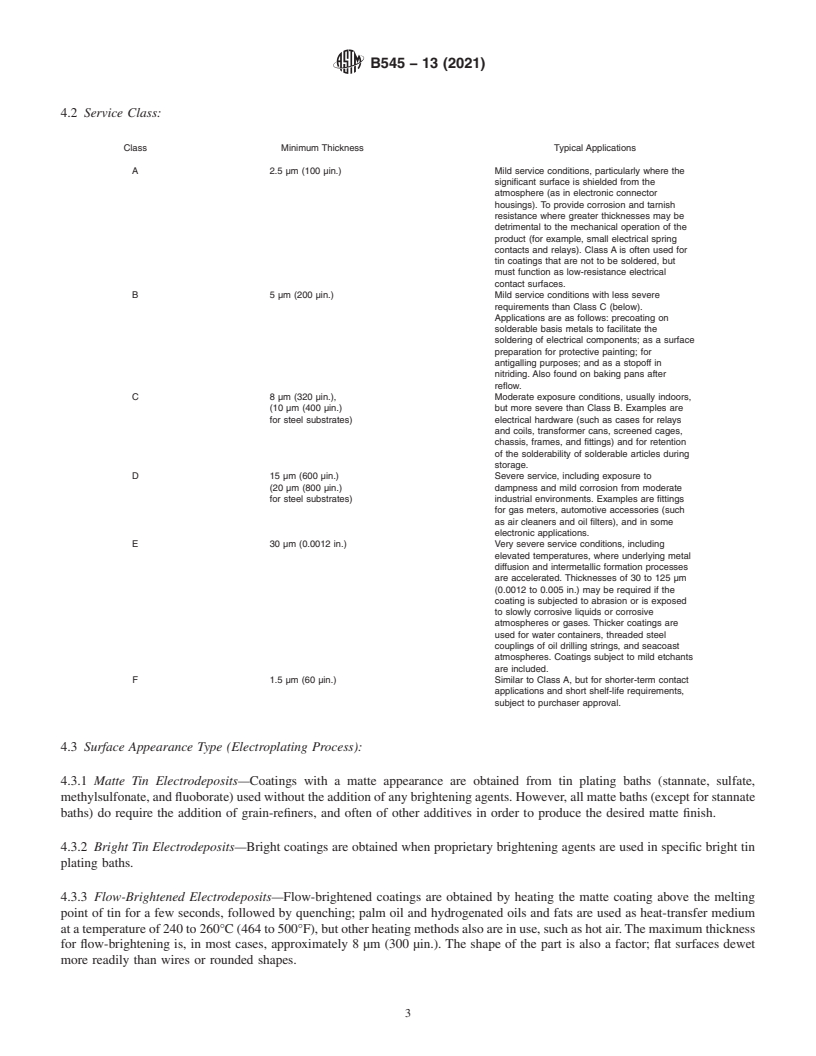
4.2 Service Class:
Class Minimum Thickness Typical Applications
A 2.5 μm (100 μin.) Mild service conditions, particularly where the
significant surface is shielded from the
atmosphere (as in electronic connector
housings). To provide corrosion and tarnish
resistance where greater thicknesses may be
detrimental to the mechanical operation of the
product (for example, small electrical spring
contacts and relays). Class A is often used for
tin coatings that are not to be soldered, but
must function as low-resistance electrical
contact surfaces.
B 5 μm (200 μin.) Mild service conditions with less severe
requirements than Class C (below).
Applications are as follows: precoating on
solderable basis metals to facilitate the
soldering of electrical components; as a surface
preparation for protective painting; for
antigalling purposes; and as a stopoff in
nitriding. Also found on baking pans after
reflow.
C 8 μm (320 μin.), Moderate exposure conditions, usually indoors,
(10 μm (400 μin.) but more severe than Class B. Examples are
for steel substrates) electrical hardware (such as cases for relays
and coils, transformer cans, screened cages,
chassis, frames, and fittings) and for retention
of the solderability of solderable articles during
storage.
D 15 μm (600 μin.) Severe service, including exposure to
(20 μm (800 μin.) dampness and mild corrosion from moderate
for steel substrates) industrial environments. Examples are fittings
for gas meters, automotive accessories (such
as air cleaners and oil filters), and in some
electronic applications.
E 30 μm (0.0012 in.) Very severe service conditions, including
elevated temperatures, where underlying metal
diffusion and intermetallic formation processes
are accelerated. Thicknesses of 30 to 125 μm
(0.0012 to 0.005 in.) may be required if the
coating is subjected to abrasion or is exposed
to slowly corrosive liquids or corrosive
atmospheres or gases. Thicker coatings are
used for water containers, threaded steel
couplings of oil drilling strings, and seacoast
atmospheres. Coatings subject to mild etchants
are included.
F 1.5 μm (60 μin.) Similar to Class A, but for shorter-term contact
applications and short shelf-life requirements,
subject to purchaser approval.
4.3 Surface Appearance Type (Electroplating Process):
4.3.1 Matte Tin Electrodeposits—Coatings with a matte appearance are obtained from tin plating baths (stannate, sulfate,
methylsulfonate, and fluoborate) used without the addition of any brightening agents. However, all matte baths (except for stannate
baths) do require the addition of grain-refiners, and often of other additives in order to produce the desired matte finish.
4.3.2 Bright Tin Electrodeposits—Bright coatings are obtained when proprietary brightening agents are used in specific bright tin
plating baths.
4.3.3 Flow-Brightened Electrodeposits—Flow-brightened coatings are obtained by heating the matte coating above the melting
point of tin for a few seconds, followed by quenching; palm oil and hydrogenated oils and fats are used as heat-transfer medium
at a temperature of 240 to 260°C (464 to 500°F), but other heating methods also are in use, such as hot air. The maximum thickness
for flow-brightening is, in most cases, approximately 8 μm (300 μin.). The shape of the part is also a factor; flat surfaces dewet
more readily than wires or rounded shapes.
B545 − 13 (2021)
NOTE 1—Terms commonly used in soldering, such as dewet, are described in soldering textbooks (1) or reviews of solderability testing (2). Some
examples are given in Appendix X6.
5. Ordering Information
5.1 In order to make the application of this specification complete, the purchaser must supply the following information to the
seller in the purchase order and drawings:
5.1.1 Title, ASTM designation number, and year of issue of this specification;
5.1.2 Deposit by classification (4.1), including thickness or service class (4.2);
5.1.3 Composition and metallurgical condition of the substrate to be coated (6.1);
5.1.4 Additional underplating, if required (6.8);
5.1.5 Surface-appearance type (for example, matte, flow-brightened, or bright), if required (4.3 and 6.2);
5.1.6 Location of significant surfaces (3.1.3);
5.1.7 Hydrogen embrittlement relief, if required (Supplementary Requirement S2); and
5.1.8 Any other items needing agreement (for example, 6.5.2, 8.4 and 8.5).
6. Coating Requirements
6.1 Substrate—The metal substrate shall be subjected to such surface preparation, cleaning, and electroplating procedures as are
necessary to yield deposits with the desired quality.
NOTE 2—Careful preparation of metal surfaces is necessary in order to assure good adhesion and quality. For suitable methods, see Practices B183, B242,
B281, B320, B322, and B558. Also see 6.6.
6.2 Electroplating shall be applied after all basis metal heat treatments and mechanical operations have been completed.
6.3 Appearance—Tin coatings shall have the characteristic appearance, including surface texture (4.3), for the process used. The
appearance shall be uniform throughout, insofar as the basis metal will permit. They shall be adherent and visually free of blisters,
pits, peeled areas, cracks, nodules, and unplated areas. They shall not be stained or discolored. Flow-brightened coatings shall be
free of dewetted areas and beads. All surfaces shall be substantially free of grease or oil used in the flow-brightening process.
6.4 All tin-coated articles shall be clean and undamaged. When necessary, preliminary samples showing the finish shall be
supplied to and approved by the purchaser. Where a contact mark is inevitable, its location shall be subject to agreement between
the supplier and the purchaser.
6.5 Thickness of Coatings—Tin coatings on articles shall conform to the thickness requirements specified in 4.2 as to the minimum
thickness on significant surfaces.
6.5.1 Local Thickness—The thickness values specified in 4.2 are the minimum local thicknesses measured by one or more of the
methods given in Practice B659 at any number of desired spots on the significant surface.
6.5.2 Mean Thickness—When specified by the purchaser, instead of being a local minimum requirement, the thickness requirement
can be a minimum (arithmetic) mean thickness.
NOTE 3—Specification of the coating thickness in terms of the mean is normally made when the coated articles are small and relatively simple, such as
connector pins and terminals.
The boldface numbers in parentheses refer to the list of references at the end of this specification.
B545 − 13 (2021)
NOTE 4—Thickness of electrodeposited coatings varies from point to point on the surfaces of a product (see Practice B507). The thickness is less in interior
c
...
Questions, Comments and Discussion
Ask us and Technical Secretary will try to provide an answer. You can facilitate discussion about the standard in here.